
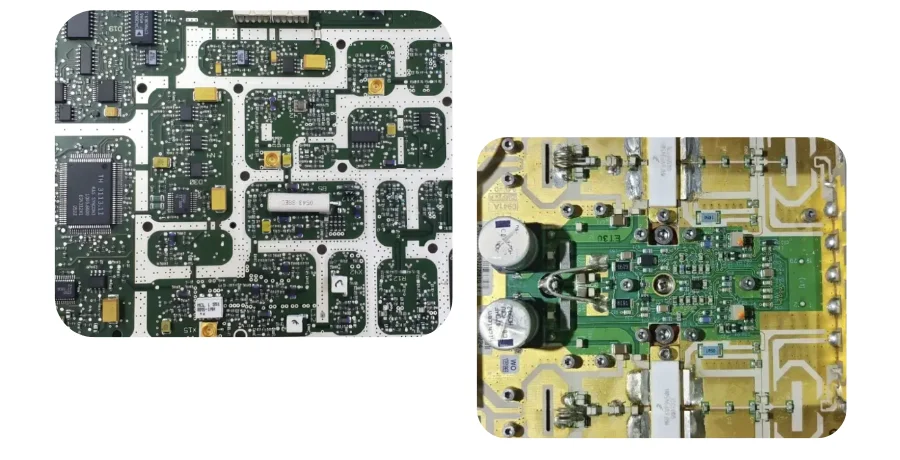
High-frequency PCB soldering must form acceptable joints while preserving the released RF geometry, component limits and material construction. The useful controls are specific: paste volume near RF launches, connector and shield coplanarity, thermal exposure, residues and the measurements required on the assembled circuit. There is no single “RF reflow profile” for every PTFE, hydrocarbon/ceramic or FR-4 board.
HILPCB’s high-frequency PCB, SMT assembly and turnkey assembly routes can coordinate the board construction with sourcing, assembly and customer-defined tests. Identify the exact laminate, package mix, alloy/flux and acceptance plan before committing to a process.
1. Understand the Material and Component Limits
Material Compatibility
Use the exact grade, thickness, copper and bonding construction. Material families do not share one CTE, moisture response or temperature limit.
- PTFE composites: RT/duroid grades have different expansion and mechanical behavior. For example, Rogers lists RT/duroid 5880 Z-axis CTE as 237 ppm/°C over 0–100°C and a TGA decomposition datum around 500°C. Neither value defines the allowed assembly profile. Use the manufacturer’s thermal data and the actual assembly limits; TGA decomposition is neither a permitted reflow peak nor a sufficient reliability criterion.
- Hydrocarbon/ceramic laminates: RO4003C and RO4350B are not PTFE. Their published Tg is above 280°C by TMA, but Tg is not the soldering temperature or an unrestricted reflow allowance. Review the complete construction and thermal exposure.
- Moisture and handling: Drying or baking must follow the applicable board, component and material instructions. A fixed 125°C/4–24-hour bake can conflict with attached parts, finishes or packaging; release the actual procedure rather than copying it from the laminate family name.
Rogers’ RO4000 and RT/duroid 5870/5880 datasheets provide grade-specific reference data. Apply the relevant fabrication and assembly guidance to the ordered construction.
Component and RF Constraints
A semiconductor’s operating junction-temperature rating is different from its permitted package reflow exposure. Check package peak temperature, time, moisture-sensitivity handling, prior heat cycles and any connector/filter/antenna restrictions.
Solder volume and component position matter where they change a launch, matching network or ground connection. Use the package and footprint requirements, not a universal ±0.1 mm placement rule. Check shield-frame and connector flatness, board support and inspection/rework access before the stencil and fixtures are made.
2. Select Solder Alloy, Flux and Paste Together
Alloy Selection
SAC305, nominal Sn96.5/Ag3.0/Cu0.5, is a common lead-free option. Kester’s SAC305 alloy datasheet lists a 217–219°C melting range. That is an alloy reference, not an SMT peak/soak recipe; use the selected paste supplier’s profile and the assembly’s component limits.
Sn42/Bi58 is a low-temperature candidate with a 138°C eutectic melting point, as described in AIM’s alloy datasheet. It can reduce required processing temperature, but the joint’s mechanical, thermal-cycle and service-temperature behavior, mixed-alloy compatibility and later rework still need review. Lower melting temperature does not automatically make it the right solder for every RF board.
Flux and Residue Requirements
Select the exact product for the alloy, finish, application method and thermal process. Record the applicable J-STD-004 classification and supplier reliability/cleaning guidance. ROL0 and ROL1 are not interchangeable labels for zero-halide material, and a classification does not by itself establish harmless RF residue.
For a no-clean route, agree where residue may remain, its effect on high-impedance/RF structures, access beneath shields and compatibility with later coating or bonding. Do not impose unsupported universal residue Dk/Df limits, solids content or a 10 GHz cleaning threshold. Verify the assembled electrical behavior over the actual band and relevant environmental conditions.
If cleaning is required, select compatible chemistry and a process that reaches the intended areas, rinses and dries them without harming parts or finishes. Bulk ionic extraction alone does not prove that every local residue or RF effect is acceptable. The IPC cleanliness discussion in J-STD-001GS-AM1 explicitly rejects the old 1.56 µg/cm² NaCl-equivalent ROSE number as the sole qualification basis; use the requirements and objective evidence for the actual process.
Paste Printing
Choose powder type, metal loading and rheology from the smallest aperture, component geometry, stencil and printing process. AIM’s powder guide lists Type 4 as 20–38 µm and Type 5 as 15–25 µm. These can be candidates for fine apertures, but a smaller powder is not automatically better; check release, oxidation and the actual paste process. Use the paste datasheet for viscosity measurement conditions, storage, thawing, open time and working life; a universal viscosity or eight-hour tack requirement is not a process specification.
3. What Flux Does and How to Apply It
Flux removes or disrupts oxides and limits re-oxidation so solder can wet the metal surfaces under the intended process. Products can contain rosin/resin, activators, solvents and other additives. Flux can be in cored wire, in the paste vehicle or separately applied before soldering. It does not remove solder metal; it can help solder wick work by improving wetting.
Rosin chemistry, no-clean process intent and water washability describe different attributes. Do not treat R/RMA/RA labels as a complete direct mapping to modern J-STD-004 classifications.
| Flux description | What to identify | Residue consideration | Cleaning decision | Example use |
|---|---|---|---|---|
| Rosin/resin based | Exact product, activity and halide classification | Residue behavior depends on formulation and thermal exposure | Follow supplier guidance and product acceptance | Hand soldering, selective soldering or rework with a suitable formulation |
| No-clean | Formulated for qualified residue retention | Not automatically residue-free or harmless under every RF/coating condition | Retain only where the process and product evidence support it | SMT or other assembly where residual flux is acceptable |
| Water-soluble | Exact chemistry and required wash window | Residues can require prompt, thorough removal | Use the prescribed wash/rinse/dry process | High-activity applications with compatible cleaning access |
For hand work, clean and prepare the joint, apply the supplier-recommended amount, heat the joint with an appropriate tip/process, feed solder and remove heat once the joint forms. Keep the thermal exposure within the part and board limits. Heavy smoke or charring is not a target process endpoint.
In production, paste supplies flux during reflow; wave or selective routes can use separately applied flux. Too little can leave poor wetting, while too much or inadequate thermal exposure can leave unacceptable residues. Fix the application method and quantity as part of the approved process, including repair operations. Follow the product SDS and local extraction requirements.
4. Develop and Measure the Reflow Profile
Start with the selected paste profile, component/package ratings, board construction and fixture. Measure representative joints and thermally extreme locations on the actual assembly; an oven setpoint is not the joint temperature.
Use the following material-specific inputs to establish the measured process window:
| Profile item | PTFE composite construction | RO4000 construction | I-Tera or another specified laminate |
|---|---|---|---|
| Ramp | Grade, assembly and paste requirements; measured hot/cold points | Same, with actual board mass and component limits | Exact grade/construction and assembly limits |
| Soak | Paste activation and assembly temperature spread | Paste activation and measured temperature spread | Selected paste and assembly requirements |
| Peak | Lowest applicable package, material or assembly limit | Lowest applicable package, material or assembly limit | Lowest applicable package, material or assembly limit |
| Time above liquidus | Actual alloy/paste requirement, measured at relevant joints | Same; not a universal time above 217°C | Same; depends on the selected alloy |
| Cooling | Joint formation, component and board constraints | Actual joint/board constraints | Actual joint/board constraints |
| Repeat heat cycles | Record previous fabrication/assembly/rework exposure | Record the released process sequence | Record the released process sequence |
A useful first-article record identifies thermocouple locations, measured traces, paste/alloy, oven recipe, support and assembly revision. If the acceptable process windows do not overlap, change the material/component/process choice rather than forcing every item through the hottest recipe.
Support and Atmosphere
A carrier or support fixture can reduce sag and handling damage, but its material, contact points and thermal mass alter the profile. Support the actual board without colliding with components or forcing it flat. Release panel and fixture drawings with the profile.
Nitrogen can reduce oxidation and change wetting, but it does not guarantee lower peak temperature, fewer residues or less tombstoning. Select atmosphere and any oxygen target from the paste/process evidence and verify the actual defect behavior. HILPCB lists nitrogen or special thermal routes after review; do not infer default vapor-phase or vacuum reflow from an RF assembly label.
5. Shields, Thermal Pads and Specialist Attachment
RF Shield Attachment
A frame soldered during reflow with a removable lid can preserve inspection and rework access. A one-piece shield has different paste, thermal and access constraints. Check the drawing for coplanarity, attachment points, lid clearance and permitted gaps; “two-stage” attachment does not automatically prevent trapped residue.
Solder volume, paste aperture and thermal relief must satisfy both assembly and the released RF ground geometry. Qualified hand or selective repair can be appropriate where access and thermal limits permit it; it is not inherently unreliable. Repeat the relevant inspection and RF checks after repair.
High-Power Parts
Define the package thermal pad, solder or adhesive bondline, isolation and heatsink/TIM interfaces separately. A TIM’s bulk conductivity alone does not establish thermal resistance, and a universal >3 W/m·K or <50 µm bondline is not appropriate for every attachment.
Paste pattern and stencil design can change outgassing, wetting and void distribution. Set the inspection method, region and limits from the component/application rather than asserting <5% vacuum-reflow voiding, <20% BGA voiding or >75% QFN coverage for every RF assembly. Vacuum-assisted processing is a separately confirmed route when trials justify it; it is not a zero-void guarantee.
Die Attach and Wire Bonding
Packaged SMT and bare-die chip-and-wire assembly are different supply scopes. Die attach, surface preparation, bond-wire process and bond integrity require appropriate equipment, materials and qualification. HILPCB’s general SMT service should not be read as a standard wire-bond or die-attach offer.
If a specialist attachment is required, define the responsible supplier and acceptance evidence. Attachment thermal resistance and wire-bond settings depend on the die, metallization, wire, geometry and equipment. Define the relevant drawing and qualified process rather than assigning one recipe to all parts. Wire bonding also has parasitics and does not automatically deliver the best RF performance.
6. Inspect the Assembly and Test the Relevant RF Behavior
SPI/AOI and visual checks: Inspect the specified paste deposits, component identity/orientation, visible joints, connector alignment, shield attachment and debris. AOI needs suitable libraries, lighting and thresholds, with first-article confirmation for unusual RF parts. Source/BOM records are needed for attributes that an image cannot verify.
Selected X-ray: Evaluate agreed hidden-joint locations for features visible to the method. Define void region/measurement and acceptance criteria. X-ray/CT does not prove every cold joint, crack or wire-bond condition; specialist investigation and destructive methods are separate scopes where justified.
ICT and functional checks: Use accessible nodes for the programmed opens/shorts/value tests and defined powered behavior. An ICT pass is not an RF performance result. Supply firmware, safe loads and fixtures for the customer-defined test plan.
RF measurements: Include S-parameters, output power, sensitivity, EVM, phase noise or temperature characterization only where the product needs them. Specify operating band, channel/power state, connectors, fixture, calibration/reference planes and limits. A bare-board impedance coupon, an assembled passive RF path and a powered radio require different tests.
7. HILPCB Assembly Scope and Project Handoff
HILPCB supports small-batch assembly, NPI and repeat production, with material/package review, paste/stencil planning, recorded reflow, SPI/AOI and selected X-ray. Programming and electrical/functional tests follow the agreed access, firmware, fixture and limits. SMT lists ISO 9001 and IPC-A-610/J-STD-001 workmanship by order; these are distinct from a claim that every radio is certified or every special process is available.
Its RF fabrication route supports material/stackup review and agreed TDR, microsection or VNA evidence. Keep that bare-board evidence separate from powered EVM/sensitivity or other radio tests. Exact test band, equipment, fixtures and reporting scope belong on the quote, rather than a blanket “RF testing to 40 GHz” assembly promise.
Send fabrication/drill files, stackup, BOM/CPL and assembly drawings, plus exact laminate/finish, solder/flux restrictions, sensitive components and prior thermal exposure. Include shield/lid sequence, connector reference planes, cleaning/coating keep-outs, package void criteria and any specialist bonding owner. For tested assemblies, add firmware, safe loads, calibration/fixture interfaces and pass/fail limits.
Ask the turnkey assembly quotation to separate fabrication, component sourcing, stencil/carrier tooling, cleaning, inspection and RF/functional tests. A pilot build can then close profile, residue, access and measurement questions before volume release, with the approved revision and records attached to the recurring order.
HILPCB offers vapor-phase and vacuum reflow options for suitable assemblies, RF testing up to 40 GHz, statistical process monitoring and documentation, and DFA optimization. The alloy, material, component limits and measured profile remain specific to the released build; IPC workmanship requirements do not constitute product or site certification.
8. Frequently Asked Questions
Can PTFE-based PCBs use lead-free reflow?
Suitable constructions can, with the selected paste, board, package and handling limits reviewed together. There is no universal 245°C maximum or 1–2°C/s ramp for every PTFE board. Measure the actual assembly profile and record the material grade and prior heat cycles.
How do flux residues affect RF performance?
Residue can change local dielectric loading, leakage or moisture behavior, depending on chemistry, location and conditions. Do not assume a fixed 2–3% impedance shift or that no-clean is harmless below 10 GHz. Qualify retention or cleaning using the actual process and relevant RF/environmental tests.
What soldering method suits an RF shield?
Follow the shield drawing and access needs. Reflowed frames with removable lids can suit volume assembly; one-piece covers and local repair need their own thermal and inspection plan. Specify paste, coplanarity and RF ground requirements rather than a universal stencil thickness.
How can 0201 tombstoning be reduced?
Review pad and copper balance, paste deposits, placement, solderability and the measured wetting/thermal sequence. A slower ramp, less paste, home-plate aperture or nitrogen is not a universal cure. Use print/profile trials and first-article inspection for the actual defect mechanism.
Should attachment adhesive be conductive or non-conductive?
Choose it for the electrical connection, heat path, mechanical load and process. Electrically conductive adhesive is not interchangeable with an insulating TIM or a solder joint. Bare-die attachment needs a specialist material/process decision and acceptance plan; it is not a default part of SMT assembly.
Which inspection methods are needed?
Select visual/SPI/AOI, hidden-joint X-ray, electrical and RF checks from the package mix and acceptance requirements. Define what each method covers, its limits and required records; neither X-ray nor a functional boot test establishes every reliability characteristic.
What does solder flux do, and does it remove solder?
Flux helps remove oxides and prevent re-oxidation so solder can wet the joint. It does not dissolve away solder metal, although it can help a desoldering wick wet and draw up molten solder. Use the product in the amount and thermal process specified by its supplier.
Is no-clean flux residue electrically safe?
It is intended to remain only under a qualified process and application. Chemistry, thermal exposure, humidity, bias, sensitive circuits and later coating matter. “No-clean,” a J-STD-004 label or a clear-looking residue alone does not establish acceptable electrical or RF behavior.