
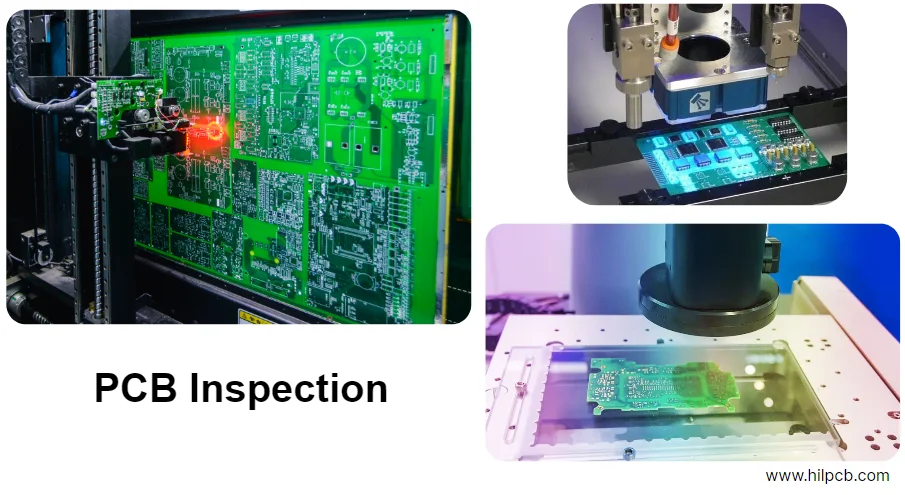
ISO 9001 provides a framework for controlling how PCB requirements become a manufactured, inspected, and released product. Its practical value is the connection between the approved design, materials, process instructions, inspection results, and action taken when something goes wrong. A QMS certificate covers an organization and a defined scope; it does not certify an individual PCB's electrical performance or field life.
ISO published ISO 9001:2026 in September 2026. Suppliers holding ISO 9001:2015 certificates need to manage the transition with their certification body; a change of edition does not by itself make every existing certificate invalid. Check the applicable certificate status and transition plan. ISO's current edition and transition guidance explains the change. Product acceptance criteria remain part of the purchase specification and quality agreement.
Understanding the ISO 9001 PCB Quality Management Framework
The process approach connects quotation, purchasing, fabrication, assembly, inspection, delivery, and feedback. Each process needs a responsible owner, usable inputs, defined outputs, and a way to evaluate whether it achieves its intended result. Automotive programs may add IATF 16949 and customer requirements; see TS 16949 PCB manufacturing for that separate scope.
Core principles: Customer focus, leadership, engagement of people, the process approach, improvement, evidence-based decision making, and relationship management guide quality management. In a PCB order, these ideas become concrete when the supplier resolves conflicting revisions, controls substitutions, and releases against the agreed criteria rather than assumptions.
Process-based system architecture: ISO 9001 does not prescribe identical shop-floor documents or software for every supplier. The amount and form of documented information depend on the activities, risks, complexity, and competence involved. A controlled electronic traveler can be useful; a large document library is not proof that the correct revision reached production.
Risk-based thinking: Material variation, outsourced processing, dense via structures, moisture-sensitive parts, limited test access, and design changes can affect conformity. The supplier and customer should resolve the relevant risks before release. Identify which findings require a drawing change, a process control, additional inspection, or explicit acceptance by the responsible engineer.
Customer satisfaction: Review complaint trends, returns, delivery performance, and customer feedback using consistent definitions. A scorecard becomes useful when a repeated issue leads to an assigned action and the next build shows whether that action worked. A low complaint count alone does not establish product reliability.
Systematic Process Control in PCB Manufacturing
A quality plan translates the design and purchase requirements into controls at the appropriate production stages. ISO 9001 calls for suitable monitoring and evaluation; it does not mandate SPC charts, a particular inspection machine, or testing every characteristic on every board.
1. Material Management and Traceability
Define the material manufacturer/grade, approved alternatives, certificate or declaration requirements, storage conditions, and the identification needed to investigate a problem. For bare boards this may involve laminate, copper, finish, and fabrication lots; assembly adds components, solder paste, moisture handling, and any customer-supplied material. Full chemical-batch or unit-level genealogy is a program requirement to agree, not a universal ISO 9001 rule.
- Incoming controls: Verify identity, condition, quantity, and the specified documentation; select additional measurements according to risk and the quality plan.
- Traceability: Define how the work order or lot links to materials and released revisions, which items need serial identification, and how long the records must be retained.
- Supplier control: Establish approved sources and substitution authority. Monitor the processes actually outsourced and communicate the same acceptance requirements to those providers.
For an investigation, a useful record answers which delivered lots used the affected material and what disposition was applied. HILPCB's assembly record options can link work orders, material lots, programs, inspection, and test status to the extent agreed for the order.
2. Production Process Standardization
Work instructions need the released construction, critical parameters, handling sequence, inspection points, and reaction to a deviation. For a high-Tg PCB, laminate grade, copper distribution, via construction, assembly exposure, and the agreed thermal evidence need to be reviewed together. The Tg label alone is not an acceptance plan.
- Revision control: Identify the approved fabrication drawing, stackup, drill data, BOM, placement data, programs, and applicable customer documents. Resolve differences before starting production.
- Parameter control: Set process limits from the material and product requirements. Distinguish an equipment setpoint from a measurement on the board or assembly.
- Quality checkpoints: Place the check where it can detect the relevant issue before later operations hide it or make correction costly. Record deviations and the authority that approves their disposition.
For example, an approved laminate substitution must be reflected in the released build information and any affected stackup or thermal review. A verbal agreement that never reaches purchasing and production leaves the process uncontrolled even if the supplier has a certificate.
3. Quality Assurance and Testing
Separate bare-board verification from assembly verification. Electrical test on a bare PCB checks the defined net connectivity; it does not test a populated board's firmware or application behavior. On an assembly, SPI checks paste before reflow, AOI checks visible conditions, selected X-ray examines agreed hidden-joint locations, and accessible electrical or functional tests answer their specified questions.
For HDI PCB builds, define the approved microvia construction and the required inspection or reliability evidence. Agree coupon, microsection, electrical, dimensional, or other tests where appropriate. For every reported result, retain the acceptance limit, method, sample identity, revision, and disposition needed to interpret it.
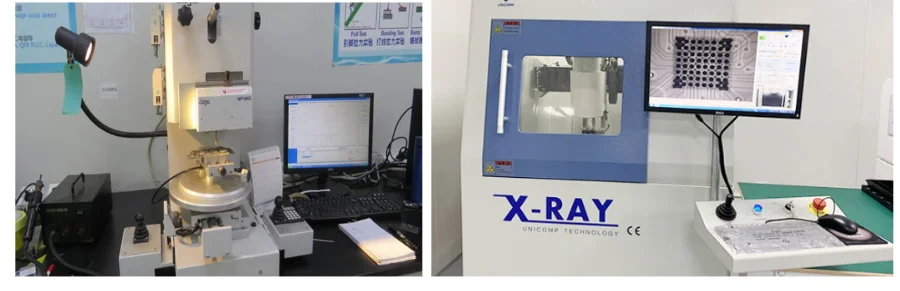
Illustration of PCB constructions; the order's quality plan defines the applicable controls and acceptance evidence.
Customer-Focused Quality Management and Continuous Improvement
Customer Requirements Management
An RFQ should resolve both the physical build and the evidence needed to release it. Before committing to a schedule, agree the design revision, materials, inspection class/revision, critical characteristics, test scope, quantities, and required records.
- Requirements review: Identify missing or conflicting data and close them with the authorized customer contact.
- DFM and design responsibility: Manufacturing review can identify fabrication or assembly risks. Product design validation remains with the assigned design authority unless a specific engineering scope is contracted.
- Change control: Define who can approve substitutions, process changes, drawing revisions, rework, or concessions, and when the customer must be notified.
- Performance reporting: Agree the metric definition, reporting interval, record format, and escalation route. Internal factory data and a customer-delivered report are different deliverables.
Statistical Quality Control and Improvement
SPC can help a stable, measurable process reveal variation. It needs a suitable measurement system, a defined sample plan, an appropriate chart, and a reaction rule. Control limits describe process behavior; product specification limits define acceptance. An in-control process can still produce out-of-specification results if it is not capable of meeting the requirement.
Track yield with its denominator and treatment of rework stated. First-pass yield, final accepted yield, defect counts, and return rates answer different questions. Comparisons across products or periods also need consistent coverage and sample size.
When a defect occurs, first contain the affected material or lots and decide their disposition. Then investigate the cause, implement a corrective action, and check its effectiveness on relevant subsequent builds. Record the owner and closure evidence. Risk controls can prevent a known failure from recurring without claiming that every future failure has been eliminated.
Employee Training and Competence
Competence depends on the operation being performed: printing, placement, soldering, inspection, test, or release. Training attendance alone does not demonstrate that an operator can perform an assigned task to the required acceptance criteria.
- Skills assessment: Identify required skills and evaluate performance for the assigned equipment, process, or inspection role.
- Training and awareness: Keep personnel aware of current instructions, product risks, and what to do when an abnormal condition appears.
- Competence evidence: Retain the relevant assessment, authorization, and training records; use industry certification where required by the contract or applicable scheme.
- Knowledge management: Carry lessons from defects, process changes, and pilot builds into updated instructions and training rather than relying on an individual operator's memory.
Manufacturing Planning, Audits, and Release Records
Supply-chain quality: Evaluate external providers for their assigned work. Approved component sourcing and alternate rules, handling of consigned material, and change notification help keep a repeat build aligned with the released BOM. A supplier audit is one possible control, selected according to risk and applicable requirements.
Production planning: Material readiness, capacity, tooling, test fixtures, approved programs, and open DFM issues affect the release date. Confirm these before treating a target delivery date as a production commitment.
Documentation and release: A useful release record identifies the product/revision and lot, applicable criteria, results, unresolved deviations or approved concessions, and release authority. Keep records accessible and protected for the agreed retention period. ISO's published guidance for the 2015 edition distinguishes information maintained to run a process from records retained as evidence; a quality manual can be useful, but it is not a universally mandated document format.
Measurement and analysis: Equipment must be suitable for the measurement. Define calibration or verification needs, reference standards where relevant, and the action to take if equipment is later found unsuitable. Review the impact on previously accepted work instead of simply attaching a new calibration label.
Internal audit and management review: Plan audits around the organization's processes and risks, and track findings through corrective action. Management review evaluates QMS performance, resources, changes, and improvement needs. The audit schedule and evidence should match the applicable edition and certification program; a customer audit and a certification-body audit serve different purposes.
HILPCB Quality Controls from Pilot to Volume
HILPCB supports manufacturing review, fabrication, SMT/THT, approved sourcing, and defined testing through the appropriate product route. For assembly, the standard placement range includes 0201 components and 0.4 mm-pitch devices, with finer packages reviewed individually. The high-speed PCB route adds stackup and impedance-control considerations, while the multilayer PCB route supports fabrication requirements from material selection through inspection and electrical testing.
For small-batch assembly, first-article evidence can include build photographs, selected inspection results, programmed-device status, test results, and open-issue disposition. Reflow-profile, SPI/AOI, selected X-ray, lot/serial traceability, and conformity records can be included as defined in the quotation and quality agreement.
For large-volume assembly, carry the approved pilot baseline forward and add the agreed sampling, serialization, change controls, forecast, packaging, and delivery requirements. HILPCB's volume route includes SPC and traceability planning; the measurements, record linkage, reporting access, and retention should be agreed for the program. A customer portal or automatic alert system is not a prerequisite for a controlled release.
Send fabrication data, stackup, BOM/AVL and placement files where applicable, quantities, end-use requirements, critical characteristics, test procedures/fixtures, and the requested evidence package. Identify required certificate/site scope, audit access, change-notification rules, and record retention. This lets HILPCB quote the manufacturing controls and deliverables needed for the order, and agree how pilot findings become the repeat-production baseline.
HILPCB also supports supplier audits, risk assessment and quality-engineering consultation, along with inventory rotation and production planning. Customer-facing services include real-time monitoring alerts, a quality portal and order-status updates, plus quality-manual and procedure documentation, customer or internal audit support, certification support, training and competency records, complaint handling, CAPA and performance reports. The applicable records and response scope are agreed for the customer’s program; ISO 9001 certification alone does not define acceptance of an individual board.
Common Questions
What is the most direct value of ISO 9001 in PCB manufacturing?
It connects requirements, supplier and process control, inspection, release, feedback, and corrective action in an auditable management system. It supports consistent execution while the purchase specification defines the individual PCB's acceptance requirements.
Does ISO 9001 make manufacturing more expensive?
Implementation, audits, and record maintenance require resources. Effective controls may reduce rework, escapes, or disruption, but the net cost depends on the program. Compare quotations using the same accepted quantity, inspection/test scope, and evidence package rather than assuming certification guarantees a saving.
What documents and records are typically needed?
The applicable edition, organization, and contract determine the required documented information. Typical PCB evidence includes requirements review, approved revisions, supplier/material controls, inspection/test results, release authority, and corrective-action records. Under the 2015 edition, a quality manual is an optional format, not a mandatory document by that name.
How often are ISO 9001 audits and improvements revisited?
Internal audits follow a planned program; certification-body surveillance and recertification follow the applicable certification arrangements. Improvement and corrective action continue between audits. During an edition transition, agree the required updates and timing with the certification body.
How can a buyer verify a supplier's ISO 9001 scope?
Check the certificate number, legal entity, manufacturing site, scope, certification body, and current validity or transition status. If accredited certification is required, verify the accreditation coverage as well. Confirm that the quoted fabrication or assembly route falls within the relevant scope and agree the product acceptance plan separately.