
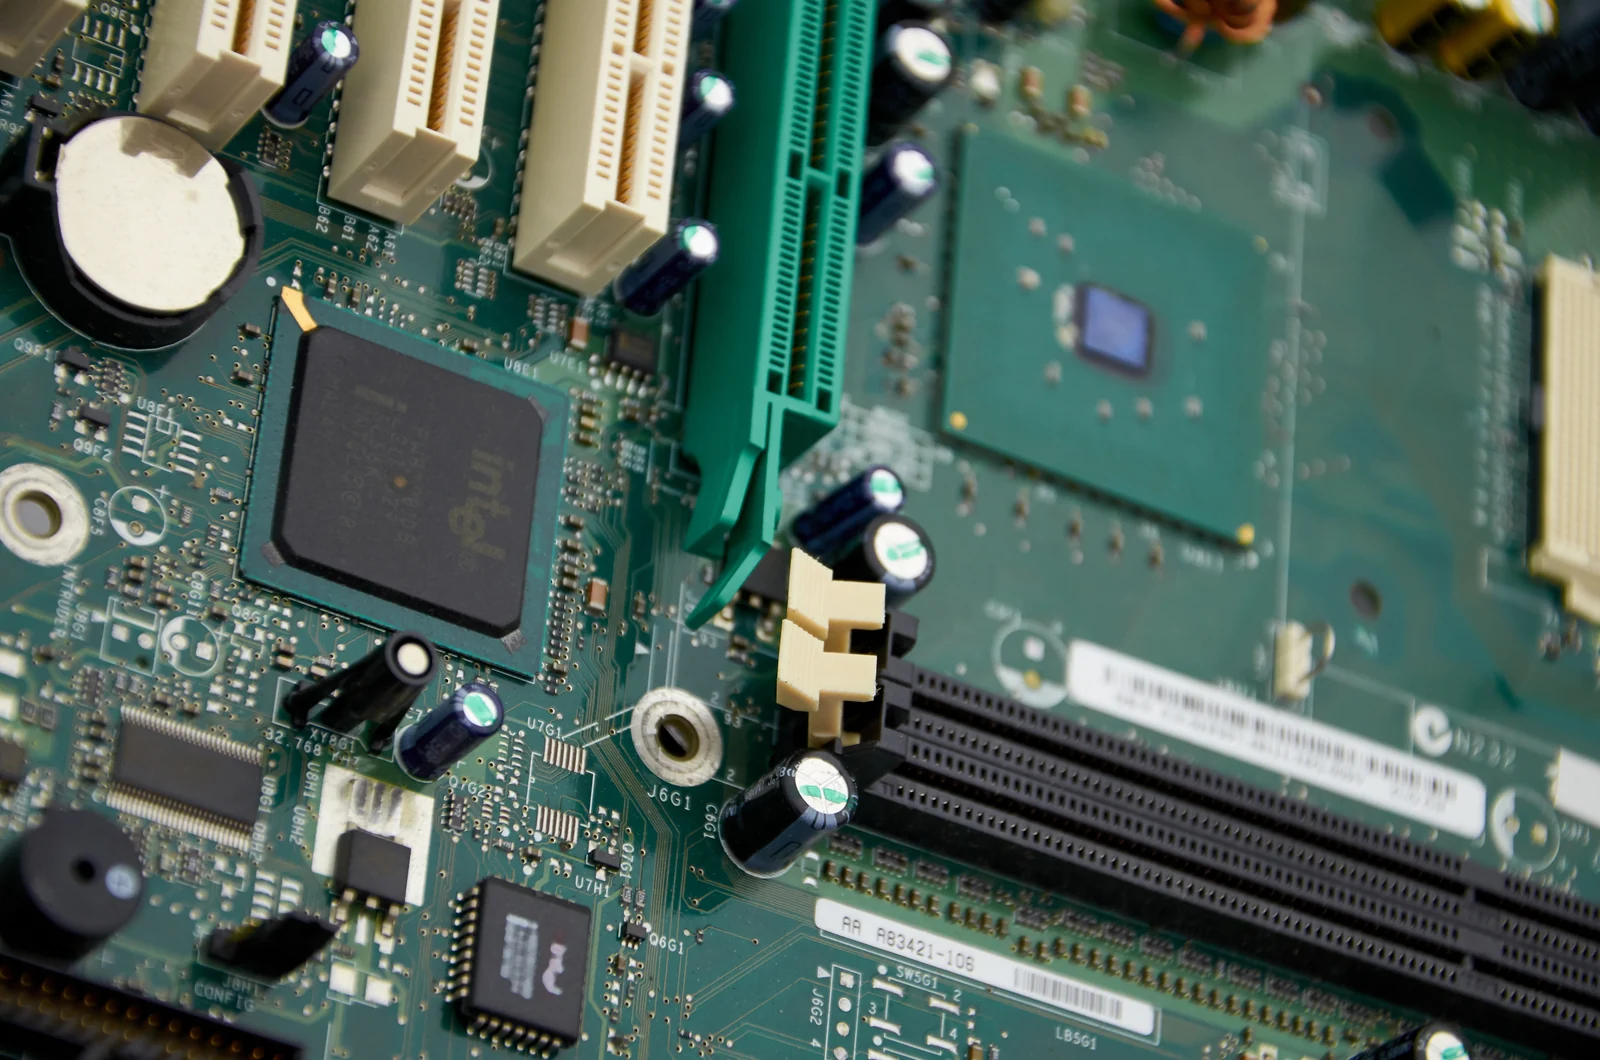
- What should be reviewed first in CXL PCB signal integrity is usually not the length of one differential segment, but whether the budget of the full link has already been decomposed into package breakout, vias, connectors, and the in-board trunk. On this kind of high-speed interconnect board, risk usually concentrates first in local transition zones rather than in the long middle trace.
- CXL is not just a slightly faster conventional high-speed board. Public material from the CXL Consortium already places CXL 3.1, 4.0, and more complex fabric and memory-expansion use cases into view, which means board-level links should no longer be reviewed with a simple point-to-point mindset.
- Low-loss material is not the only answer. The final result is also shaped by dielectric thickness, copper roughness, glass style, lamination window, and lot-to-lot consistency.
- A CXL stackup has to serve impedance, return path, PDN behavior, and board-shape stability at the same time. If stackup is frozen only from an SI model, pilot build and mass production can easily drift away because of lamination, tolerance, and assembly conditions.
- The validation target should not be that one sample board passes once, but that multiple boards, multiple lots, and post-assembly conditions still follow the same channel logic.
Quick Answer
The core of CXL PCB signal integrity is not forcing a differential pair to one nominal impedance number. It is keeping budget allocation, stackup, tolerance, transition zones, and the validation matrix aligned in real manufacturing. For server motherboards, add-in cards, and memory boards, identifying local risk first is usually more effective than trying to rescue the design later by changing materials.
Table of Contents
- What should engineers review first on a CXL PCB?
- Summary table of key rules and parameters
- Why must channel budget be decomposed down to local transition zones first?
- Why must low-loss material and stackup geometry be judged together?
- Why do vias, connectors, and assembly windows consume margin first?
- Why is production validation about consistency instead of one passing board?
- Next steps with HILPCB
- Frequently Asked Questions (FAQ)
- Public references
- Author and review information
What should engineers review first on a CXL PCB?
Start with budget decomposition, stackup and materials, local transition zones, PDN coordination, and the validation matrix.
This question does not mean "controlled impedance is enough," and it does not mean "if simulation passes the eye, the board is ready for production." The public CXL specification landing page already gives access to specifications and white papers, and the CXL 3.1 white paper further discusses fabric capability, global integrated memory, security, and memory-expander RAS. That means CXL links increasingly serve a more complex platform context instead of a single device-attach case. On the PCB side, the first thing to confirm is which part of the full link is actually consuming budget, and whether those risks can be reproduced stably in manufacturing.
Before layout freeze, the five most useful questions are usually:
- How much budget is consumed separately by package breakout, vias, connectors, and the in-board trunk
- Whether the current stackup and material system matches the target generation and channel context
- Whether local transition zones have already been reviewed under real manufacturing conditions
- Whether high-speed layers, PDN, and large copper areas could change board shape and return behavior together
- Whether validation covers multiple boards, multiple lots, and post-assembly states
If the project is a server motherboard, a CXL add-in card, or a memory board, it is usually better to bring the interface and process windows of High-Speed PCB and Backplane PCB into the review early instead of assuming an ideal channel only inside the simulation model.
Summary table of key rules and parameters
| Rule / Parameter | Recommended range or judgment method | Why it matters | How to verify | What happens if ignored |
|---|---|---|---|---|
| Budget decomposition | Split package, via, connector, and in-board trunk contributions first | The most dangerous loss and reflection often sit in local structures | Channel budget, TDR, S-parameter comparison | Problems appear, but the main source stays unclear |
| Material and stackup | Judge low-loss material together with dielectric thickness, tolerance, and lamination | Nominal Dk / Df is not the same as finished-board stability | Datasheet, stackup review, sample comparison | Simulation passes, but production drifts clearly |
| Transition zones | Review via, backdrill, anti-pad, and launch together | Transition zones often lose control before long routes do | Local simulation, TDR, cross-section | The long trace is fine, but the interface loses margin first |
| PDN coordination | Freeze high-speed, return, and power layers in the same review round | Large copper zones and power structure change real link conditions | Joint PI/SI review, board-shape check | Prototype passes, but pilot variation grows |
| Assembly window | Check connector coplanarity, board warp, and local flatness early | They directly change real launch behavior | First-article check, assembly review | The sample is barely usable, production is unstable |
| Validation matrix | Judge consistency across boards and states, not only one board | A CXL platform delivers repeatability | Multi-board comparison, thermal and post-assembly comparison | The golden sample is good, production loses yield |
| Public platform context | Direct implication for board-level design |
|---|---|
| CXL fabric / pooling / memory expander | Board-level links are increasingly platform interconnects rather than simple short links |
| OIF 112G electrical interconnect | Budget cannot be estimated from long traces alone; transition-zone loss becomes visible faster |
| OCP modular server architectures | Board-to-board, MCIO, PCIe 5.0, and similar interfaces become bottleneck areas more easily |
Why must channel budget be decomposed down to local transition zones first?
Conclusion: Because the main risk on a CXL board often does not come from the longest section, but from the shortest and most complex section.
The CXL 3.1 white paper already places fabric capability, global integrated memory, and memory-expander use cases into the open context. That means the board-level link is no longer only a simple "one chip to one connector" problem. At the same time, OIF's public discussion of 112G electrical interconnect keeps pointing to the same issue: the higher the frequency, the less you can treat local transitions as small errors.
The budget items worth decomposing first usually include:
- Package breakout and escape zones
- Via, backdrill, and anti-pad structures
- Connector launches and board-to-board interfaces
- In-board trunks and local reference-plane changes
If this step is skipped, even when a channel later shows weak margin, it becomes hard to tell whether the real issue is a trunk that is too long, a transition that is too poor, or a connector region that already consumed the remaining margin. For projects with board-to-board interconnect or dense high-speed interfaces, it is also better to compare budget against the local-structure windows of High-Speed PCB and Backplane PCB instead of estimating only from rule-of-thumb length.
Why must low-loss material and stackup geometry be judged together?
Conclusion: Because the real channel condition of the finished board depends on whether material parameters and geometric tolerance can be reproduced together.
Many CXL projects lose control late not because the team chose the wrong material name, but because the Dk / Df values on the datasheet were treated as the fixed reality of the finished board. The actual result is also affected by dielectric thickness, copper roughness, glass style, lamination shift, and lot consistency. A nominally low-loss material system still creates a fragile channel if lamination and modeling cannot stay stable over time.
More useful early questions usually are:
- Whether this material system and stackup can be reproduced stably in the current process
- Whether dielectric thickness and impedance geometry sit inside a window that can be held long term
- Whether glass style and copper foil will amplify skew or local variation
- Whether the same material system still fits the current high layer count and connector density
If the project has already moved into a high-layer-count structure, it is usually worth judging the lamination and impedance windows of Multilayer PCB and High-Speed PCB together instead of making separate decisions on stackup and material.
Why do vias, connectors, and assembly windows consume margin first?
Conclusion: Because these local structures stack the largest number of discontinuities inside the shortest distance.
Via stubs, anti-pads, capture pads, connector launches, board-to-board interfaces, local return-path changes, and coplanarity deviation after assembly can all appear within a very short structure. On a CXL board, these locations usually amplify reflection, insertion loss, and board-to-board spread earlier than the mid-route traces do.
The points worth confirming first are usually:
- Which critical paths must control residual stub or require backdrilling
- Whether connector launches have already been reviewed under real assembly conditions
- Whether local reference-plane changes have been idealized too aggressively
- Whether board warp, coplanarity, and post-assembly flatness will change the real interface condition
If the project is close to first-board validation, it is usually better to push key transition zones, edge interfaces, and flatness requirements into the PCB Prototype stage rather than trying to repair them only during bring-up. If the design will move to volume assembly later, the assembly boundaries of SMT Assembly should also be included in the high-speed review.
Why is production validation about consistency instead of one passing board?
Conclusion: Because what a CXL board really has to deliver is not the best condition of one sample, but a process window that is wide enough.
For server boards, expansion cards, and memory boards, a sample that boots successfully only proves that one version worked under one assembly event. It does not automatically prove that the next lot, the next assembly build, or hot operating conditions will stay stable. A useful release method should be defined around consistency instead.
The more valuable validation path usually includes:
- Bind package, via, connector, and trunk budget into the same validation link.
- Compare differences across different bare boards and different assembly lots.
- Observe consistency in thermal condition, post-assembly state, and local interface zones.
- Tie material lots, stackup revisions, and abnormal board results into the same traceability record.
- Arrange local structural analysis or failure analysis for abnormal boards.
If the project has already entered pilot build, it is usually better to put these checkpoints directly into a Quote / RFQ or pilot-validation matrix rather than judging maturity only from a single-board test result.
Next steps with HILPCB
If you are currently working on a CXL accelerator card, memory-expansion board, switch board, or another high-speed interconnect board, the next step is usually to turn "the link works" into "the design is manufacturable."
- When the main issue is channel budget and interface regions, first use the High-Speed PCB and Backplane PCB paths to converge connectors and transition structures.
- When the project has already entered high layer count and high-density interconnect, check the stackup and lamination boundaries of Multilayer PCB at the same time.
- When key risk is concentrated in vias, edge zones, or connector launches, moving those checkpoints into PCB Prototype exposes issues earlier.
- When high-speed validation and assembly consistency need to move together, organizing the related inputs into SMT Assembly or Quote / RFQ is usually more effective.
Frequently Asked Questions (FAQ)
Is ordinary controlled-impedance practice enough for a CXL PCB?
A: No. CXL has already moved into a platform context with fabric, pooling, and more complex host, switch, and memory-device structures. Risk now sits simultaneously in budget decomposition, interface zones, and production consistency.
Why is the most dangerous area in a CXL project often not the long trace?
A: Because local transition zones combine vias, backdrill, connectors, board-to-board structures, and assembly variation. The shorter structure often consumes link margin first.
Is low-loss material always better than a more stable conventional option?
A: Not always. If the material is more aggressive but lamination, tolerance, and modeling stay unstable over time, production results can actually become worse. CXL boards value low variation, not just low nominal loss.
If the sample board runs, why can production still be unstable?
A: Because a sample usually does not fully expose losses from connector coplanarity, board warp, backdrill variation, local solder consistency, and lot-to-lot differences.
What is most worth freezing before fabrication?
A: Freeze budget decomposition, stackup and material, critical transition zones, the validation matrix, and traceability logic first. The later these are frozen, the higher the board-spin cost.
Public references
CXL Specification Landing Page
Supports the article's statement that the CXL Consortium publicly provides a specification access point and evaluation-copy context.Introducing Compute Express Link 3.1: Significant Improvements in Fabric Connectivity, Memory RAS, Security and More!
Supports the article's public explanation that the CXL 3.1 white paper discusses fabric capability, global integrated memory, security, and memory-expander RAS.OIF Releases Common Electrical I/O CEI 5.0 Implementation Agreement
Supports the article's explanation of the public context around OIF 112G electrical interconnect.Flex Modular Compute Platform | Open Compute Project
Supports the article's public statement that the OCP Flex platform is oriented toward AI and HPC systems and aligns with OCP DC-MHS 2.0.
Author and review information
- Author: HILPCB High-Speed Interconnect Content Team
- Technical review: PCB process, SI, and DFM engineering team
- Last updated: 2026-05-16