
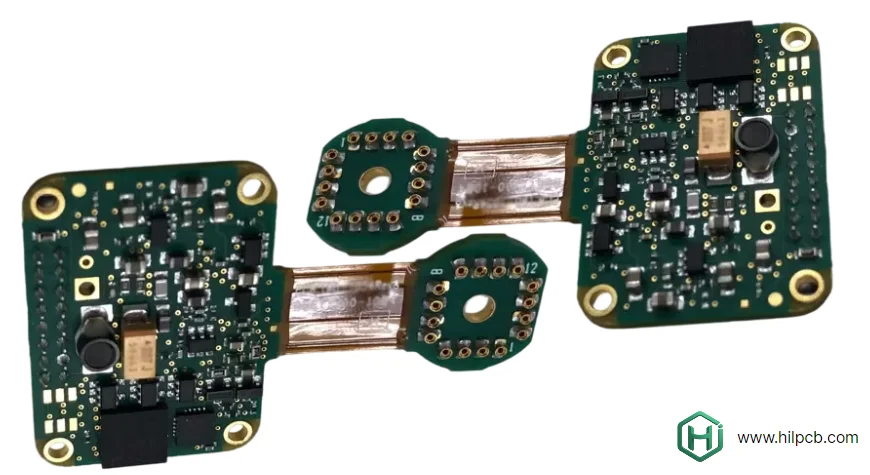
Rigid-flex assembly combines flexible interconnects with regions that must remain stable during printing, placement, soldering and testing. The eight problems below give a diagnostic framework; root causes and process limits depend on the released stackup, components, support and intended bending conditions. Record failures against those inputs before changing the process.
Problem 1: Board Warpage During Reflow
The Problem
Potential warpage-related problems during reflow include:
- Flex sections expand differently than rigid
- Causes component tombstoning or shorts
- Automated optical inspection (AOI) failures
- Rework or scrap adds cost and can require renewed acceptance checks
Diagnostic evidence: Compare supported and unsupported board shape through the actual thermal cycle, component displacement, solder defects and inspection images. An AOI reject can reflect an actual defect or an unstable viewing geometry; investigate before treating all rejects as warpage damage.
Root Causes
- Thermal expansion mismatch (polyimide vs FR4)
- Inadequate fixturing during reflow
- Inappropriate reflow profile for mixed construction
- Board design with unbalanced copper distribution
Complete Solution
1. Design-level prevention:
- Review copper balance within the actual rigid/flex stackup; preserve required flex compliance and signal returns
- Use symmetrical stack-ups when possible
- Add stiffeners in critical areas
- Define component and stiffener keepouts from the actual transition geometry and bend envelope; no universal 3 mm rule applies
2. Fixturing requirements: Where the assembly cannot remain stable unaided, use a carrier as in flex PCB assembly. Review:
- Support both rigid and flexible sections
- Prevent warpage without restricting thermal expansion
- Suitable tape or compliant pads with qualified temperature, cleanliness, ESD and residue behavior
- Temperature-stable fixture materials (ceramic or high-temp polymers)
3. Reflow profile optimization: Verify the candidate profile on the actual construction and carrier:
- Keep ramp, soak and cooling within the solder-paste, component, laminate and adhesive limits
- Reach the solder-joint wetting window while respecting package-body and board limits
- Do not extend time above liquidus merely as stress relief; extra exposure can damage materials or joints
- Measure representative joint, package and board temperatures rather than relying on oven settings
For SMT assembly, agree the profiling method, support arrangement, limits and acceptance evidence for the released build. Profiling can identify process risk; it does not guarantee the absence of warpage.
Problem 2: Component Placement in Flex Sections
The Problem
Components exposed to flex strain can develop:
- Solder joint cracks from flexing stress
- Component body stress causes fractures
- Adhesion failures under mechanical stress
- Intermittent or permanent failures under the actual bend and service exposure
Place soldered components outside the intended active bend region. The risk depends on local strain, package, attachment and cycling; no universal failure-rate multiplier is established here.
Where You Can Place Components
Acceptable locations:
- ✓ Rigid regions that meet package, thermal, clearance and transition keepouts
- ✓ Locally stiffened component regions kept outside the active bend
- ✓ Non-bending flex regions where support and local strain have been qualified
Prohibited locations:
- ✗ Unsupported component regions within the intended active bend
- ✗ Locations where the formed or moving flex loads solder joints or component bodies
- ✗ Components straddling the rigid-to-flex transition
Solutions and Best Practices
Redesign recommendations:
- Move components to rigid sections (ideal solution)
- Add qualified local stiffeners so the populated region remains outside the active bend
- Use flexible adhesives for attachment (special applications)
- Select packages compatible with land geometry, strain, support and inspection
When components must go on a flex substrate:
- Keep the populated region mechanically stable and define the allowed bend outside it
- Choose packages, lands and support from local strain and assembly requirements, not a universal size or mass cutoff
- A surface-mounted component is not placed at the flex stackup’s neutral axis; reduce strain through placement and support
- Qualify any adhesive or underfill for thermal expansion, cure, cleanliness and rework
- Define installation bends separately from repeated motion, with actual radius, direction and cycle requirements
Component orientation and spacing:
- Review orientation against actual board strain and attachment loads; rotating a package does not make an active bend safe
- Avoid components straddling the rigid-flex boundary
- Set spacing from lands, assembly access, insulation and the qualified stiffened region
Include component placement, bend envelopes and support in the assembly DFM review to identify and reduce risks before manufacturing begins.

Problem 3: Handling Damage
The Problem
Rigid flex PCBs damaged during assembly handling:
- Stress concentrations at transitions cause cracking
- Excessive bending damages circuits
- Rough handling tears flex sections
- Latent damage that may escape initial visual inspection
Cost impact: Record actual scrap, rework, additional inspection and schedule effects against the board revision and handling step.
Damage Mechanisms
Transition zone stress:
- Improper handling creates sharp bends at rigid-flex interface
- Causes copper cracking invisible to visual inspection
- Failures appear during electrical testing or in field
Flex section tears:
- Catching on fixtures or equipment
- Pulling during board loading/unloading
- Insufficient support during manual operations
Contamination:
- Handling residues can introduce ionic or other contamination
- Flux residues in flex sections harder to clean
- Incoming contamination or bond defects under coverlay, which need fabrication review separately from assembly residues
Handling Procedures
Required protocols:
- ESD protection: Follow the control plan for the assembly’s electrostatic-sensitive parts
- Clean handling: Use suitable gloves or handling tools under the cleanliness and ESD plan; avoid contaminating contacts and solderable surfaces
- Support technique: Support entire board during handling
- Bend prevention: Do not bend tighter than the specified minimum radius; follow the defined bend direction and sequence
- Edge grabbing only: Hold by rigid sections, not flex areas
Specialized fixturing:
- Custom pallets supporting specific board geometry
- Soft padding under flex sections
- Positive location features preventing movement
- Quick-release mechanisms avoiding pull stress
Training requirements:
- Assembly personnel need rigid flex-specific training
- Visual examples of proper/improper handling
- Practice with scrap boards before production
- Refresher training based on process changes, observed errors and the quality plan
Track damage by handling operation and compare results after a controlled change. No factory or industry-wide damage-rate benchmark is established by the procedures listed here.
Problem 4: Solder Paste Application Challenges
The Problem
Stencil printing difficulties on rigid flex boards:
- Height variations between rigid and flex sections
- Inadequate paste volume in flex areas
- Excessive paste in rigid areas
- Print quality variations cause assembly defects
Typical issues:
- Solder bridges (excess paste)
- Insufficient solder or opens from inadequate paste; poor wetting or a cold joint also requires thermal/material investigation
- Tombstoning (uneven paste distribution)
Step Stencil Solution
First check: Establish stable board support, stencil-to-land contact, aperture release and deposited volume. Possible solution: A step stencil can address differing deposit requirements when a uniform thickness cannot meet them; it is not mandatory for every rigid-flex assembly.
Step stencil design:
- Choose thickness and apertures from package lands, required deposits and paste release
- Correct flex deflection with support rather than automatically adding solder volume
- Provide suitable step-to-aperture clearance and verify stencil contact in each region
- Validate actual deposited volume and repeatability; no universal rigid/flex thickness pair applies
Cost consideration: Quote the stencil, support tooling and process-development work for the actual build. Compare the alternatives against printing capability and defect data rather than a universal price premium.
Alternative Approaches
Selective paste dispensing:
- Consider controlled dispensing where stencil access is unsuitable
- Specify deposit volume, location and inspection
- Qualify repeatability for the actual package and volume; manual application is not automatically acceptable
Printer adjustment:
- Set pressure, speed and separation from paste, stencil and support behavior
- Confirm which adjustments the actual printer supports
- Do not assume independent pressure control over rigid and flex zones
Support fixtures:
- Back-support under flex sections during printing
- Limits deflection during the squeegee pass when properly supported
- Verify support access and contact against components and printed regions
Process Verification
Critical checks:
- Solder paste inspection (SPI) after printing
- Volume measurements in flex vs rigid sections
- Choose repeatability samples across relevant board, paste and setup variation
- Use calibrated paste inspection; 2D coverage alone does not establish deposited volume
For turnkey assembly, include the released land pattern, paste/stencil requirements, support and inspection plan in the manufacturing handoff.
Problem 5: Thermal Profiling Difficulties
The Problem
Potential thermal-profile problems include:
- Rigid and flex regions can heat differently because of copper, components, support and airflow
- Temperature gradients create stress
- Component damage from overheating flex areas
- Cold joints in thick rigid sections
Profiling Strategy
Multi-zone measurement:
- Monitor temperature in rigid section (thickest area)
- Monitor temperature in flex section (thinnest area)
- Monitor critical components (both locations)
- Adjust profile to keep all within acceptable window
Profile limits to establish:
- Preheat and soak from the actual paste chemistry and thermal distribution
- Ramp rate permitted by the components, substrate and adhesives
- Time above the selected alloy’s liquidus within the validated soldering window
- Peak joint temperature sufficient for soldering while package bodies and board materials remain within limits
- Cooling rate consistent with component and material requirements
Oven configuration:
- Disable aggressive zones if possible
- Balance top and bottom heating
- Consider nitrogen where paste/process evaluation justifies reduced oxidation; it does not remove mechanical thermal stress
Validation Testing
Process verification:
- Thermocouples on representative hot/cold joints, packages and board regions with the actual support; attachment must not materially change the measured process
- Multiple runs to verify consistency
- Cross-section analysis of sample joints
- Mechanical tests only with a defined method and acceptance limit; destructive tests require representative samples
Problem 6: Inspection Challenges
The Problem
Inspection coverage can be limited by:
- Flex sections may fold over (hiding defects)
- Transition zones difficult to inspect optically
- Manual handling required for full inspection
- AOI systems confused by flex section movement
Inspection Solutions
Visual inspection requirements:
- Arrange access to both sides within the allowed bend sequence and radius; do not repeatedly unfold a formed assembly merely for inspection
- Magnification and lighting sufficient for the selected workmanship criteria and feature size
- Transition zone verification (cracking, delamination)
- Component orientation and presence verification
AOI programming:
- Custom programs for rigid flex geometry
- Teach system expected flex section positions
- Manual verification points at transitions
- Distinguish fixture/location variation from actual workmanship; do not widen defect acceptance limits merely to suppress false calls
X-ray inspection:
- Select views and resolution for the hidden solder features and defect types
- Check whether stiffeners or overlapping structures obscure the required view
- Assess projected void area separately from volume or joint integrity
- Do not infer that X-ray detects every via crack, non-wetted interface or transition defect; sections or other methods may be needed
Electrical testing:
- Define electrical test coverage and assembly inspection or sampling according to product class, risk and the agreed quality plan
- Flying probe for prototypes
- Custom bed-of-nails fixture for production
- Dielectric-withstand testing only where the actual insulation requirements specify voltage, duration, connections and acceptance; the medical label alone is insufficient
Problem 7: Rework Limitations
The Problem
Rigid flex PCB assembly rework more difficult than standard boards:
- Heat application risks damaging flex sections
- Difficult to access components near transitions
- Board support challenging during rework
- Multiple rework cycles cause progressive damage
Assess recoverability from the defect, material condition, prior thermal/bend history, access and approved repair method. No universal success-rate comparison is established here.
Rework Best Practices
Prevention focus:
- Better to get it right first time
- Invest in process optimization upfront
- Thorough DFM review before assembly
- Prototype validation before production
When rework necessary:
- Assessment: Determine if rework feasible
- Fixturing: Proper support preventing damage
- Temperature control: Measure a rework profile that reaches the required joint condition while protecting adjacent parts, flex and adhesives; a universally lower temperature may leave solder unmelted
- Time limits: Minimize heat exposure duration
- Inspection: Thorough post-rework verification
Rework restrictions:
- Set allowed thermal cycles from component/material limits, recorded history and qualified repair criteria
- Treat transition damage as an engineering disposition; do not repair it by unqualified local heating or bending
- Document all rework (traceability)
- Additional testing required post-rework
When to Scrap Instead
Consider scrapping rather than rework if:
- Damage to transition zones
- Multiple defects requiring extensive rework
- Critical/high-reliability application
- Cost of rework exceeds replacement cost
Problem 8: Testing Access Limitations
The Problem
Test point access difficult on rigid flex:
- Flex sections may fold over test points
- Transition zones limit test probe access
- Board support during testing challenging
- A generic test fixture may not provide the required support and access
Testing Solutions
Design considerations:
- Place test points in rigid sections when possible
- Avoid test points in flex sections or at transitions
- Consider test pads on both sides if necessary
- Design for fixture accessibility
Fixture design:
- Custom fixtures matching exact board geometry
- Support flex sections without restricting access
- Probe positioning, travel and support matched to actual pad geometry and allowable board strain
- Quick-change capability for different variants
Alternative testing methods:
- Flying probe (slower but flexible)
- Boundary scan (if components support)
- Functional testing against defined states, loads and fault coverage; passing it does not validate every possible assembly behavior
- Combined methods for best coverage
For turnkey assembly, agree test access, fixtures, revision control, coverage and records. A fixture or test name alone does not establish complete fault coverage.
Preventing Problems Before They Start
Design Review Process
Submit designs for assembly-focused DFM review:
- Component placement verification
- Thermal profiling feasibility
- Test point accessibility
- Handling considerations
- Fixturing requirements
Prototype Validation
Recommended approach:
- Choose prototype quantity to cover setup variation, profiling, functional checks and any destructive analysis
- Validate complete assembly process
- Identify any issues early
- Optimize before production
- Document lessons learned
Evidence to retain:
- Defect type and location against stackup, support, paste and profile revisions
- Results before and after controlled process changes
- Remaining coverage limits, disposition and released production settings
Assembly Partner Selection
HILPCB can review rigid-flex component placement, bend regions and support requirements, develop a custom reflow profile, and optimize handling, paste and stencil setup. Configuration-specific fixture design and agreed testing can be coordinated with fabrication and turnkey assembly through final test. Eligible design-analysis requests receive an initial engineering response in 4–8 hours; profile, strain, inspection and rework scope remains specific to the released construction and assembly.
Critical capabilities:
- Rigid flex experience (not just standard PCB)
- Custom fixturing capability
- Process development support
- Quality documentation
- Responsive engineering support
Frequently Asked Questions
Can a conventional PCB assembler handle rigid-flex?
Assess the actual site’s experience with the construction, support fixtures, thermal profiling, handling and test access. Relevant first-article evidence is more useful than the label “standard” or “specialist”; neither label establishes a success rate.
What assembly cost premium should I expect?
Request a build-specific quote separating recurring assembly, tooling, stencil, process development, inspection and test costs. Panel format, package mix, handling and quantity affect the result. No universal 25–50% premium or automatic rework saving is established.
Should one supplier handle fabrication and assembly?
An integrated scope can simplify communication, while separate qualified suppliers may also work. In either case, define ownership of stackup changes, material condition, panel/support geometry, land patterns and nonconformance decisions. Confirm the actual fabrication and assembly sites and their released handoff records.
What volume justifies custom fixtures?
Use a fixture whenever the actual printing, placement, soldering or probing process needs controlled support, including a prototype if necessary. Compare tooling cost and lead time with measured process capability and damage risk; there is no universal unit-count threshold.
How can I separate a design issue from a process issue?
Compare the released geometry and material requirements with measured board shape, paste deposits, temperatures, placement and defects. Change one controlled input at a time where practicable, retain revision/lot records and involve both fabricator and assembler. DFM can identify risks, but does not prove the cause of every failure before manufacture.
For a HILPCB enquiry, provide the rigid-flex stackup, bend definition, assembly drawings, BOM, process history and defect evidence. Agree the supplying site’s review scope and response schedule. Altium’s rigid-flex assembly guidance discusses construction-specific transition keepouts, fixturing and thermal distribution; these are review inputs, not universal geometry or profile limits.