
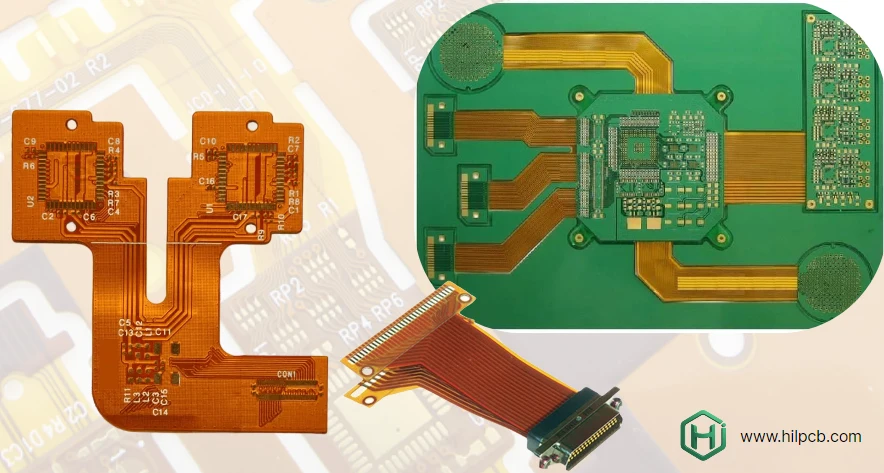
A rollable PCB is a flexible circuit engineered to roll and unroll repeatedly around a controlled radius while maintaining conductor, dielectric, interconnect and signal performance. It is a dynamic-flex system: the complete stackup, motion path, terminations and environment determine life.
Key Takeaways
- Distinguish flex-to-install, occasional service flex and continuous rolling; they need different strain and test margins.
- Minimize bend-zone thickness and copper distance from the neutral axis. Bend radius cannot be selected from one universal multiplier.
- Rolled-annealed (RA) copper is commonly preferred for dynamic flex, but foil thickness, grain direction, plating and process history also matter.
- Keep components, vias, pads, stiffener edges and abrupt width changes outside the rolling zone.
- A static controlled-impedance coupon does not prove a rolled high-speed link; validate impedance and loss in representative bend states.
- Specify roll radius, angle, travel, tension, speed, dwell, cycle count, temperature and electrical monitoring in the RFQ.
Define the Rolling Duty Cycle
“Flexible” is not a motion specification. Record the complete kinematics before stackup design.
| Duty type | Typical behavior | Main design focus |
|---|---|---|
| Flex-to-install | Bent once or a few times, then held | Assembly radius, permanent set and rigid-flex transition |
| Service flex | Moved during maintenance or occasional use | Handling variability and connector/stiffener protection |
| Dynamic flex | Repeated bending over a defined path | Cyclic strain, copper fatigue and resistance monitoring |
| Roll/scroll | Circuit wraps around a mandrel or moving spool | Changing contact arc, tension, tracking and compact packaging |
The motion specification should include minimum and nominal radius, bend direction, angle/travel, whether curvature reverses, neutral-axis path, moving length, speed, acceleration, tension, torsion, dwell and expected cycles. Define start/end packaging, cable guides and abrasion surfaces; the PCB cannot control a poorly constrained mechanism.
Engineer the Stackup Around Strain
For a simple homogeneous strip, outer-fiber strain increases roughly with thickness and decreases with bend radius. Real flex stacks are composite structures, so copper, polyimide, adhesive, coverlay, shielding and plating shift the neutral axis and local strain.
Dynamic sections should be as thin and simple as the electrical design allows. Polyimide films in gauges such as 12.5 µm and 25 µm are available, but finished thickness includes copper, adhesive, coverlay and processing. An adhesiveless copper-clad laminate can reduce thickness and remove one adhesive interface; this is an option, not proof of cycle life.
| Stackup choice | Benefit | Trade-off to validate |
|---|---|---|
| RA copper | Elongated grain structure is favorable for repeated flex | Grain direction, plating and supplier data must match bend path |
| Thin copper such as 0.5 oz | Lower bending stiffness and conductor strain | Current capacity, voltage drop, etch tolerance and handling |
| Single/double flex layers | Keeps dynamic section thin | Routing, shielding and return-path limitations |
| Symmetric construction | Can place conductors nearer the neutral axis | Added films may increase total thickness |
| Cross-hatched shield/plane | Improves flexibility versus solid copper | Impedance, EMI, current and manufacturability change |
Do not state that electrodeposited copper always fails or that RA copper guarantees a fixed life multiplier. Use foil and laminate supplier properties, then validate the production construction.
Lay Out the Rolling Zone to Avoid Fatigue
Route conductors perpendicular to the bend axis so each trace follows the intended curvature. Use smooth arcs, consistent widths and generous transitions; avoid acute corners, neck-downs and copper-density steps. Stagger traces between layers rather than stacking them directly when the construction allows.
Keep plated holes, microvias, pads, test points, components, solder joints and connector tails outside the dynamic region. If a feature must enter a bend, treat it as a separately qualified exception. Prevent coverlay openings or stiffener edges from terminating at the highest-strain line.
At rigid-to-flex transitions, remove sharp housing edges and provide a gradual, controlled support change. Teardrops and fillets can reduce local stress at pad-to-trace junctions, but they do not repair an undersized radius or uncontrolled motion.
Preserve Power and Signal Integrity While Rolling
Thin copper improves flexibility but increases resistance and heating. Calculate each power path at operating current and temperature, including allowable drop and duty cycle. Use parallel conductors only when current sharing and bending geometry remain controlled; a solid plane may be electrically attractive but mechanically too stiff.
Controlled impedance depends on trace geometry, dielectric, reference structure and coverlay. Bending changes layer spacing and field distribution, especially with cross-hatched references or asymmetric stacks. High-speed display, camera or sensor links require channel analysis in relevant flat and rolled states, including connector and rigid-flex transitions.
Shield films, conductive adhesives and metal meshes add stiffness and can become fatigue initiators. Define EMI performance and bend life together. Do not copy rigid-board differential rules without a flex material model and production stackup.
Separate Components from the Dynamic Region
Place ICs, passives and connectors in rigid, stiffened or non-moving islands whenever possible. The component exclusion boundary must include solder-joint strain, pick-and-place support, reflow pallet access and housing tolerance—not only the package outline.
Stiffeners support connectors and assembly loads but create a stiffness step. Specify material, thickness, adhesive, edge geometry, registration and distance from the rolling path. If a display or sensor laminate shares the roll, coordinate its neutral axis with the FPC, adhesive, protective film and mechanical carrier at the system level.
Assembly fixtures must keep thin flex flat without creasing or stretching. Define panel rails, temporary stiffeners, carriers, depaneling, cleaning, handling and shipping form. A circuit damaged before installation cannot recover during life testing.
Validate the Production-Intent Motion
Cycle testing must reproduce the actual mechanism rather than repeatedly folding a loose coupon by hand.
| Test input | What to control |
|---|---|
| Mechanics | Mandrel/guide geometry, radius, travel, reversal, tension, alignment and speed |
| Environment | Temperature, humidity, contamination and dwell as applicable |
| Electrical | DC resistance, intermittent opens, insulation and powered signal/eye/BER metrics |
| Samples | Production stackup, panel location, assembly, connectors and mechanism tolerances |
| Failure analysis | Cycle/time, event threshold, cross-section and crack/delamination location |
Use continuous or high-rate resistance monitoring because a crack may open only during part of the motion. Establish baseline resistance versus bend position before endurance testing. After cycling, inspect copper, plated transitions, coverlay, adhesive and connector regions; a final continuity pass can miss intermittent fatigue.
High-speed circuits should run a representative pattern or periodic channel test during motion. Thermal and humidity tests may be combined only when the acceleration model is justified; arbitrary combined stress can create a failure mode that the product never sees.
Use a Rollable PCB Release Matrix
This matrix ties mechanical life to manufacturable evidence.
| Gate | Controlled inputs | Evidence | Reject when |
|---|---|---|---|
| Concept | Motion envelope, radius, cycles, environment and electrical loads | Strain-risk and architecture review | Mechanism forces components/vias into the rolling zone |
| Stackup | Film, adhesive, foil, plating, coverlay and shielding | Supplier data plus neutral-axis/strain model | Production tolerance exceeds strain margin |
| Layout | Bend axis, traces, exclusions, transitions and stiffeners | Artwork overlay against mechanism CAD | Abrupt stiffness or copper discontinuity lies in peak strain |
| Prototype | Production-intent FPC, connectors and guides | Resistance/channel data through bend positions and cycles | Intermittent events or drift precede required life |
| Pilot | Released materials, panel process, assembly and fixture | Yield, dimensions, cross-sections and endurance sampling | Lot/process variation breaks prototype correlation |
| Change | Material, foil, plating, adhesive, artwork or mechanism revision | Impact review and targeted requalification | Prior life evidence no longer represents the product |
Common Rollable PCB Failure Modes
| Symptom | Likely cause | Next check |
|---|---|---|
| Resistance spikes only while moving | Copper fatigue or connector/transition motion | Position-correlated high-rate continuity monitoring |
| Cracks repeat at one line | Guide edge, stiffener edge or local stackup step | Overlay failure location with mechanism and artwork |
| Coverlay wrinkles or lifts | Compression buckling, adhesive/process or too-tight radius | Inspect inner/outer bend surfaces and lamination data |
| High-speed link fails only when rolled | Impedance/reference geometry changes or transition crosstalk | Measure flat versus defined radii at common planes |
| Units track sideways on spool | Mechanism alignment, asymmetric stiffness or torsion | Measure tension and edge position through travel |
Rollable PCB RFQ Checklist
Motion/mechanics: flat and rolled CAD, radius range, bend axis/direction, travel, speed, tension, reversal, guides, abrasion, torsion, cycle target and packaging.
Fabrication: Gerber/ODB++/IPC-2581, stackup, polyimide/adhesive/RA copper requirements, foil grain direction, finished thickness, coverlay, shield, stiffeners, tolerances, controlled impedance and coupons.
Assembly/test: BOM, static component zones, carriers, connectors, current/data rates, environment, cycle fixture, monitoring bandwidth, failure threshold, sample plan, cross-section and change-control requirements.
Reference Standards and Responsibility Boundaries
- IPC-2221 — IPC
- IPC-2223 — IPC
- IPC-6013 — IPC
- IPC-4202 — IPC
- IPC-4203 — IPC
- IPC-A-610 — IPC
The applicable IPC revision, class, material slash sheet and acceptance criteria must be written into the purchase documentation. IPC design guidance does not guarantee the customer's cycle target.
HILPCB can fabricate and assemble flex or rigid-flex data and support stackup, bend-zone, panelization and test-access review. The product owner remains responsible for mechanism design, strain/life model, material approval, high-speed performance in motion, system qualification and industry-specific safety or regulatory compliance. Quoted dynamic-test scope and equipment must be confirmed per project.
How HILPCB Supports Rollable Builds
HILPCB can review finished flex thickness, copper/coverlay balance, bend-axis routing, via/component exclusions, stiffener transitions and assembly carriers. Flexible PCB manufacturing supports released flex constructions, while rigid-flex PCB manufacturing integrates stable component regions with flexible interconnects. Turnkey PCB assembly is available when component, fixture and handling controls are defined.
FAQ
What is the difference between a rollable PCB and a standard flex PCB?
A rollable PCB is qualified for repeated controlled rolling. A standard flex may only bend during installation. The material can be similar, but motion, stackup, layout and endurance evidence differ.
What minimum roll diameter can a rollable PCB achieve?
There is no universal value. Finished thickness, copper layers, foil, coverlay, shielding, bend direction, cycles, temperature and mechanism determine it. Specify the required diameter and validate the production stackup.
Is rolled-annealed copper mandatory for dynamic flex?
RA copper is commonly preferred because its grain structure favors repeated bending, but the released foil, grain direction, plating, thickness and process still require validation. Do not rely on the label alone.
Can components be placed in the rolling zone?
They should normally be kept in static or stiffened areas because packages and solder joints create stiffness and strain concentration. Any unavoidable component in motion needs a dedicated mechanical and life qualification.
Conclusion
Rollable PCB reliability comes from a controlled motion path, thin strain-aware stackup, fatigue-resistant conductor design and production-intent cycle evidence. Send HILPCB the motion CAD, stackup, electrical loads, assembly zones and test specification for a flex DFM and quotation review.