

An AI server motherboard, accelerator card and backplane have different packages, signal paths, power and mechanical requirements. Start cost optimization by identifying the build item and its approved acceptance limits. A lower bare-board price is useful only when material, fabrication, assembly, test and release requirements are compared on the same basis.
HILPCB's backplane, high-speed PCB and turnkey assembly routes provide construction and service options for that comparison. Use DFM/DFA to price feasible alternatives, then obtain design-owner approval for changes to materials, geometry, packages or test coverage. The objective is a repeatable accepted build at a defensible total cost.
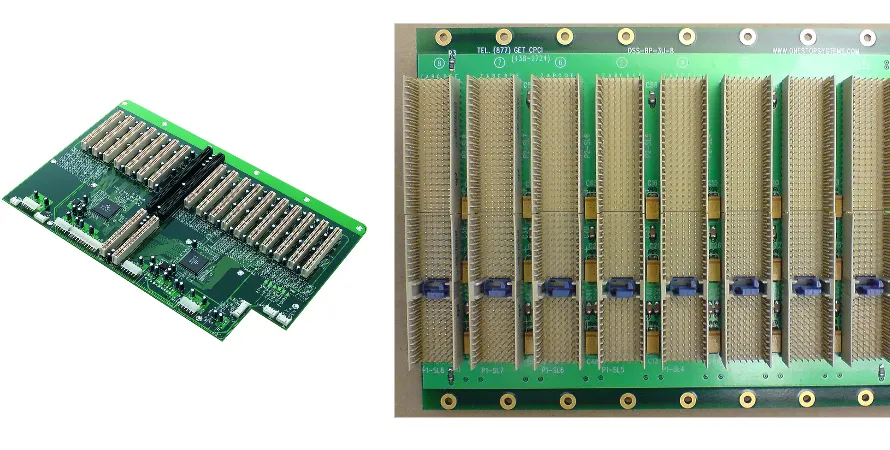
Cost structure and optimization levers for AI server backplanes
Separate recurring fabrication, components, assembly, inspection/test, scrap/rework and logistics from one-time engineering, tooling, fixtures and qualification. Compare candidate quotes at the same revision, volume, delivery basis and acceptance scope.
- Material: Exact laminate/prepreg, glass/resin construction, copper profile, thicknesses, approved alternates and purchase availability affect cost. A 224G label alone does not select one family or price multiplier.
- Layer/construction complexity: Layers affect material, handling, drilling and yield. Conventional multilayer construction does not necessarily add a lamination cycle for every extra layer; sequential build-up and buried structures can add distinct cycles.
- Via operations: Mechanical holes, microvias, filling/capping, blind/buried connections and controlled-depth back-drilling have different costs and constraints. Back-drilling is not itself an HDI build-up technology.
- Tolerance: Order the impedance, trace/space, hole and registration limits actually needed. Geometry, copper, materials, metrology and acceptance must be feasible together.
- Testing: Separate netlist/coupon acceptance, assembly inspection, ICT/boundary scan/FCT and channel or environmental qualification. Hi-pot is ordered where the insulation requirement calls for it, not automatically for every server board.
For a hypothetical recurring fabrication comparison, candidate A at $120 per started board with 88% accepted output gives $120/0.88 ≈ $136.36 per accepted board. Candidate B at $128 with 94% accepted output gives ≈ $136.17. These assumed costs/yields illustrate the denominator; they are not HILPCB results or forecasts. Add setup, rework, assembly, test and other in-scope costs consistently, and use measured pilot evidence rather than an optimistic yield assumption.
High-speed material selection: balancing performance and cost
Select material from the actual channel length, loss/skew/return-loss budget, transitions, copper profile and equalization. PCIe 5.0's 32 GT/s or PCIe 6.0's 64 GT/s do not by themselves define one laminate. HILPCB's high-speed route includes I-Speed and advanced Megtron 6/7/Tachyon 100G options; use the exact construction and approved data rather than a universal material-to-generation ladder.
A hybrid stackup can be worth quoting when lower-loss material is needed only in part of the construction. Identify every dielectric participating in the signal field, including adjoining prepregs, and account for the reference-plane configuration; a power/ground layer label does not automatically make its dielectric electrically irrelevant. Model the complete cross-section and transitions before changing a material.
Compare the hybrid and uniform builds for laminate/prepreg availability, resin flow, bonding/press compatibility, expansion/registration, reliability requirements, drilling and panel yield. Extra engineering or qualification can offset a lower material bill. There is no universal 30–50% saving; quote the two released constructions and their test requirements at the same quantity.
Ask the review to identify the exact material/foil and cross-section behind each quote, proposed changes, process dependencies and required validation. A lower-loss family name is not a substitute for that construction data.
Stack-up design: a cost-effective path to signal integrity
Stackup review can expose routing or material changes that reduce total cost, but removing a reference or power layer can increase routing complexity, noise, copper requirements or validation work. Compare the complete manufacturable alternatives.
- Balance: Review layer/copper balance and lamination construction against bow/twist and assembly support requirements; apparent symmetry alone does not prevent distortion.
- References: Set signal/reference spacing and geometry together for impedance and fields. A thinner dielectric changes coupling, capacitance, manufacturability and insulation conditions; it is not an unconditional improvement.
- Adjacent signal layers: Orthogonal routing can reduce long parallel overlap, but does not replace suitable reference planes, spacing and crosstalk modeling.
- PDN allocation: Choose power/ground planes with the regulator, capacitors, vias, connector and load model, including resonances and return transitions.
HILPCB can review the stackup against actual material, copper, hole and panel routes. Its high-speed envelope lists 2–20 layers standard and up to 48 advanced; the separate backplane route lists 16–32/up to 64. Use only the combination needed by the design. Standard high-speed geometry includes 75/75 µm, with 50/50 µm advanced review and ±10% standard/±5% advanced impedance options; 3/3 mil is not inherently beyond that standard screen.
High-speed PCB materials: performance vs. cost
| Construction Candidate | Representative Options | Loss Input | Cost Comparison | Approval Basis |
|---|---|---|---|---|
| General FR-4 | Exact approved grade | Selected grade/construction at modeled frequency | Actual recurring cost plus material availability | Control/short routes only where the complete budget fits |
| High-Tg FR-4 | S1000-2M or IT-180A, by approved construction | High Tg does not establish mid/low loss | Include assembly/thermal and reliability requirements | Verify grade, glass/resin and process compatibility |
| Mid-loss numeric example | FR408HR, Isola Rev E | Df 0.0095 typical at 10 GHz, Bereskin stripline | Compare quoted construction; no fixed 2–3× multiplier | Use exact current construction and channel model |
| Other controlled-loss candidates | I-Speed; IT-968G or Megtron 4S with exact suffix/grade review | Use each manufacturer's frequency/method/glass/resin data | Include process/qualification/supply differences | Candidate families are not automatically interchangeable or stocked |
| Lower-loss/hybrid options | Megtron 6/7 or Tachyon 100G, by route | Compare copper loss and complete dielectric model | Price uniform and hybrid alternatives at equal scope | Use channel length/transitions/equalization and release evidence |
The FR408HR example uses the manufacturer's Rev E typical table at 10 GHz. Relative material prices and complete-board costs need current comparable quotes; no fixed price index establishes the best channel construction.
Via technology simplification: cost tradeoffs from VIPPO to backdrill
Via transitions can consume routing area and channel margin. Compare the fabrication and assembly requirements of the actual holes, not just a technology label.
- Controlled-depth back-drilling: Removes an unused portion of a plated through-hole from an accessible side. Price the number of entries/depth groups, diameter, remaining stub, connected-layer clearance and verification. It may be economical where the through-hole escape and residual stub meet the channel.
- Via-in-pad filled and capped/plated-over: Specify the actual hole, fill, cap and finished pad requirements. VIPPO can apply to a mechanical through-hole as well as an HDI structure; it does not automatically mean laser drilling or multiple build-up cycles.
- Blind/buried/microvias: Use where the package escape and construction justify them, with defined stack, fill, lamination and reliability requirements. Do not assume one route is always cheaper or electrically better.
Compare two or more feasible routes:
- Keep through-hole/back-drill as a candidate when it meets escape, access and channel limits.
- Use HDI where the released package/routing needs it and verify whether the required build-up operations affect the whole panel. Local dense routing does not necessarily localize every manufacturing cost.
- Tune pad/antipad, reference continuity and return vias with the model. Larger antipads change capacitance and available plane copper; an electrical improvement still needs geometry and manufacturing review.
Understanding high-speed PCB manufacturing details (see High-Speed PCB) helps you make better design decisions.
PDN robustness and cost optimization
Power rails on motherboards, accelerator cards and backplanes have different load and conversion locations. Define the voltage excursion, transient/current waveform, frequency range, drop and temperature limits before comparing capacitor or copper changes.
- Target impedance: Allocate the allowed voltage excursion across regulator/DC/AC behavior and the applicable frequency range, then verify the complete network.
- Capacitors: Compare actual bias-dependent capacitance, ESL/ESR, mounting and location. A mixture of values can create resonances; verify any part/count reduction against the model and measured load cases.
- Plane capacitance: Include dielectric thickness, area, vias and useful bandwidth. It is not free or a universal replacement for MLCCs; stackup changes can affect impedance, insulation and fabrication.
- Copper: Size the complete supply/return path, vias, neckdowns, contacts and terminations for current/drop/thermal limits. 3 oz is not a universal rail minimum, and a simulation alone does not verify finished geometry.
Record the approved capacitor list, copper construction, load profile and test results so a recurring BOM saving does not hide revalidation, rework or an unacceptable voltage/thermal margin.
PDN cost-optimization checklist
- Target-driven design: allocate allowed rail variation across the actual PDN and frequency range.
- Hierarchical decoupling: verify bias, mounting, resonances and required load cases before changing the capacitor set.
- Leverage plane capacitance: compare useful plane capacitance with the stackup, impedance and insulation constraints.
- Precise copper planning: combine current/drop/thermal modeling with finished copper, via and contact requirements.
- Optimize return paths: ensure low-inductance return for all power paths to reduce noise.
Thermal management strategy and its impact on TCO
Thermal cost belongs to the installed assembly and its workload: component losses, TIM, heatsink/contact, airflow and allowable temperatures. A backplane carrying power need not dissipate the accelerator card's full heat. Compare the baseline cooling solution and any proposed change at the same load and acceptance conditions.
Thermal alternatives to compare:
- Heat paths: Follow the package's pad/electrical potential and soldering requirements through copper/vias/interfaces to the cooling boundary. Include via-fill/cap, TIM and mounting costs.
- Special construction: Coins or other local thermal paths can be quoted where they solve a real hotspot. Do not assume they eliminate active cooling; validate the revised installed temperature/airflow configuration.
- Material: High-Tg PCB options can address a thermal/process requirement. Tg is not conductivity or a guaranteed operating/lifetime rating; select the complete construction.
Assembly review should define TIM material/application, contact pressure, hardware/torque and heatsink alignment along with safe rework and test access. A lower-cost cooling part can introduce fixture or labor costs elsewhere.
How DFM/DFA reduces manufacturing cost at the source
Early DFM/DFA reviews can identify stackup, drill, panelization, part-placement and test-access constraints before release. This may reduce redesign effort and unplanned tooling costs, but savings require comparison against a documented project baseline.
Key DFM/DFA review points:
- Capability: Compare the actual standard/advanced geometry, copper, holes, registration and measurement requirements. Avoid a tighter tolerance with no system need, but keep limits that the approved design requires.
- Panelization: Compare boards per production panel, rails/coupons, spacing, copper balance, tooling and handling. Maximum geometric nesting is not automatically the best accepted-panel yield.
- Test access: Reserve feasible contacts, ground returns, isolation and fixture-clearance areas for the intended ICT/FCT/boundary-scan plan. Package, firmware and host/load dependencies also affect coverage.
- Placement: Coordinate support, stencil, side sequence, thermal mass, connector/press-fit access and rework. The cheapest placement choice may increase fixture, inspection or test cost.
Agree the proposed alternatives and their approval/verification work before manufacture. HILPCB can connect fabrication, sourcing, SMT/THT and available test/record routes to that released package without treating every DFM suggestion as an automatically approved electrical change.
🤝 Expert-level DFM/DFA collaboration workflow
Resolve construction, assembly and test-readiness questions before tooling, with proposed changes approved and tracked.
Customer completes schematic and PCB layout and prepares manufacturing outputs.
Deliver Gerber, ODB++, or native design project files to HILPCB.
Review actual stackup, geometry, holes, panel/support, package and test access against the selected route.
Provide engineering suggestions on trace width/spacing, panelization, and component selection.
Approve updated files and open-issue disposition, then release the agreed first article or pilot before repeat production.
Test strategy optimization: from Fixture design (ICT/FCT) to boundary scan
Compare test cost with its defined defect/function coverage and release role. Bare-board connectivity, workmanship, assembled connectivity/function and channel/environmental qualification require different access, hardware and evidence.
Layered coverage: Bare-board netlist testing and any coupons verify selected fabrication requirements. SPI/AOI and selected X-ray inspect different assembly features. ICT needs the appropriate access/fixture and limits. Boundary scan can reach supported digital connections when the parts, scan chain, device data and test description allow it; it is not the only method or a universal test of all hidden joints. FCT uses supplied firmware, loads/peers, procedures and limits for the chosen functions/modes.
Fixture economics: Include engineering, interface/load hardware, contacts, maintenance, debugging, operator handling and retests. As an explicit assumption, an additional $1,200 fixture that saves $2 per accepted unit at unchanged coverage breaks even after 600 accepted units, before maintenance, finance or revision costs. A forecast below that quantity may favor the simpler route; a design change can invalidate the comparison.
Automation: Measure total load/connect/program/acquire/analyze/retest/report time. ATE can reduce recurring labor when the build and coverage are stable, but setup, fixtures, software validation and revisions remain costs. Quote prototype and repeat stages separately.
Traceability/MES and lifecycle cost control
Useful traceability links the build revision, material/lot, process and test evidence at the agreed granularity. Define capture, ownership and retention so the record package supports actual failure analysis and change control.
- Process and yield: Select relevant characteristics, measurement systems and work-order records. Track defects, rework and accepted output consistently when comparing candidate costs.
- Investigation: Link available lot/serial, material, process, inspection and test data to a failure. A barcode or MES label alone does not identify root cause.
- Scope and retention: Specify delivered fields, format, access and retention, including rework/retest and authorized deviations. Customer warranty/use data need their own linkage and ownership.
HILPCB's quoted records can include first-article results, profile records, SPI/AOI summaries, selected X-ray images, programming/ICT/FCT results and lot/serial linkage. Include the required evidence in both the baseline and alternative quotes.
HILPCB provides mixed-laminate control and co-design support for qualified backplane builds. Its MES can record process drift, operators, equipment and suppliers in real time, with full production traceability. The service also includes thousands of software DFM checks and reporting. These tools support review and records; they do not authorize an automatic design change or guarantee a particular cost reduction.
Prepare Comparable Fabrication and Assembly Quotes
Send the released fabrication/drill/stackup and impedance data, BOM/approved alternates, placement, mechanical/panel requirements and quantity/forecast. Identify the motherboard, backplane or power assembly; mark critical channels, finished holes/back-drill, copper/current/thermal limits and package/support constraints.
For each candidate, request the same scope and list proposed changes to material, construction, via route, sourcing or test. Include NRE/tooling, fixtures, recurring fabrication/assembly/test, expected acceptance basis and the validation needed to approve the change. Use pilot evidence to update the cost comparison.
HILPCB can quote backplane fabrication, high-speed construction and turnkey assembly against that package. For tested assemblies, supply firmware, device/scan data where needed, peers/loads, fixtures, procedures, limits and required records. Enclosure/harness/thermal mounting work can connect to box-build assembly when included in the order.
Agree the approved construction, BOM, assembly/test revisions and disposition of open issues before repeat release. That gives procurement a comparable cost basis and engineering a build that can be reproduced.