
Every number on a laminate data sheet is the output of a specific test: a method, a specimen construction, a frequency or temperature, and a pass criterion. A field solver, a reflow profile and a purchase order each need a different input. Most stackup surprises come from moving a value from one context to another without carrying its test conditions along.
The 20 questions below follow that chain from electrical inputs to fabrication, reliability and purchasing. Impedance examples use the Hammerstad–Jensen microstrip equations with zero-thickness copper and no solder mask. All worked tables can be recalculated with the downloadable calculation.
Quick index
| No. | Question | Data-sheet field | What the field cannot tell you |
|---|---|---|---|
| 1 | Impedance mismatch vs. simulation | Dk, thickness | Which of Dk, pressed height or width moved |
| 2 | Process Dk vs. design Dk | Dk method, frequency | Applicability to your thickness and foil |
| 3 | Effective permittivity in the solver | Dk | Geometry; ε_eff is a solver output |
| 4 | Low Df, high insertion loss | Df, foil profile | Conductor and roughness loss |
| 5 | Glass weave skew | Glass style, resin content | Trace position over bundles |
| 6 | Resin content and flow | RC %, flow % | Pressed thickness on your copper pattern |
| 7 | Pressed thickness ≠ sum of sheets | Nominal PP thickness | Copper fill and press loss |
| 8 | Mixed lamination | Cure cycle, CTE | Bond compatibility of the pair |
| 9 | Tg vs. Td | DSC/TMA/DMA, TGA | Service rating or reflow survival |
| 10 | Comparing two Td numbers | Mass-loss criterion | Equivalence across criteria |
| 11 | T260 / T288 | TMA time to delamination | Circuit life |
| 12 | Z-axis CTE | α1, α2, % expansion | Barrel strain on your aspect ratio |
| 13 | CAF | CAF test conditions | Your hole-wall spacing and drilling quality |
| 14 | Moisture and baking | Absorption % | Bake schedule for a finished board |
| 15 | Laser-drill compatibility | Resin/glass construction | Your laser type and window |
| 16 | CTI and dielectric strength | IEC 60112, kV/mm | Creepage/clearance for your product |
| 17 | Flex: PI and copper | Peel, flex endurance | Bend radius and duty cycle |
| 18 | MCPCB thermal conductivity | W/m·K | Thermal resistance of your dielectric |
| 19 | Compliance declarations | RoHS, halogen-free, REACH | Status of the finished assembly |
| 20 | Comparing supplier proposals | All of the above | Equivalence of constructions |
Part 1: Electrical properties and model inputs
1. Why does measured impedance differ from a simulation based on data-sheet Dk?
Take a 50 Ω microstrip designed with Dk 4.2 and a 0.20 mm dielectric. The synthesized width is about 0.40 mm. The coupon TDR reads 46 Ω. The common explanation is that "Dk drops at high frequency", but it points the wrong way:
| Case (W = 0.40 mm) | h (mm) | Dk input | Z₀ (Ω) | ε_eff |
|---|---|---|---|---|
| Design basis | 0.200 | 4.2 | 50.0 | 3.20 |
| Lower Dk only | 0.200 | 3.8 | 52.2 | 2.93 |
| Thinner pressed dielectric only | 0.175 | 4.2 | 46.0 | 3.24 |
| Both | 0.175 | 3.8 | 48.1 | 2.96 |
A lower Dk raises microstrip impedance. A 46 Ω reading fits a pressed dielectric about 25 µm thinner than modeled, or a wider etched trace, or a higher Dk at the TDR rise-time bandwidth. One impedance number has several unknowns and cannot pick between them. Before blaming the laminate, ask for the cross-section of the coupon (dielectric height, trace top/bottom width, copper thickness) and re-run the solver with those measured dimensions. Whatever error remains after that belongs to the material input.
2. Why does a data sheet list a "process Dk" and a "design Dk"?
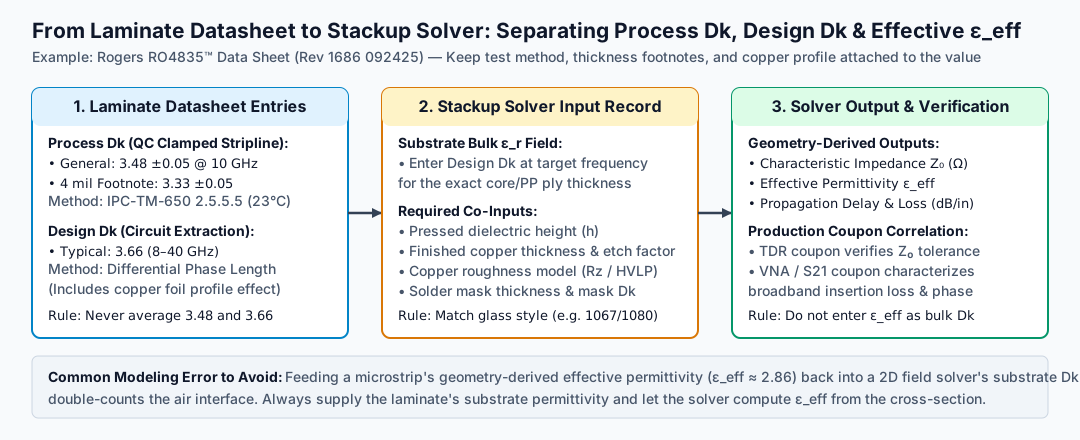
They come from different tests. The Rogers RO4835 data sheet (printed revision 1686 092425, p. 2) lists:
| Entry | Value | Conditions | Method |
|---|---|---|---|
| Process Dk | 3.48 ± 0.05 | 10 GHz, 23 °C | IPC-TM-650 2.5.5.5 (clamped stripline) |
| Process Dk, 4 mil core | 3.33 ± 0.05 | 10 GHz, 23 °C | Same method; thickness exception |
| Design Dk | 3.66 | 8–40 GHz | Differential Phase Length on circuits |
The clamped-stripline value characterizes the laminate for quality control. The design value is extracted from fabricated transmission lines, so foil roughness and construction effects are folded into it. Rogers states the design value is averaged across lots and common thicknesses. Both are typical data, not a purchase guarantee. For a solver, use the design value when your construction matches its basis. Check the thickness row, because the 4 mil core has its own entry. Never average 3.48 and 3.66, and do not attach the ±0.05 tolerance from the process row to the design value. The model-input record shows how to log each entry with its method.
3. Should microstrip effective permittivity be typed into the solver's Dk field?
No. Effective permittivity ε_eff is what the solver computes from the bulk Dk and the geometry. In Question 1, a bulk Dk of 4.2 produced ε_eff = 3.20 because part of the field runs through air. Entering 3.20 as the material Dk counts the air twice and shifts the predicted width. The one exception is a tool field that explicitly asks for a measured ε_eff of a particular line.
4. Why is insertion loss still high on a low-Df laminate?
Total loss has a dielectric part and a conductor part. A first-order estimate of the dielectric part is α_d ≈ 2.3 · f[GHz] · Df · √Dk dB/in. At 14 GHz (the Nyquist frequency of 28 Gbaud NRZ) with Dk 3.7:
| Df | Dielectric loss (dB/in) | Over 10 in (dB) |
|---|---|---|
| 0.020 | 1.24 | 12.4 |
| 0.010 | 0.62 | 6.2 |
| 0.004 | 0.25 | 2.5 |
Moving to Df 0.004 removes most of the dielectric term, and what remains is copper. Skin depth in copper is about 0.66 µm at 10 GHz, so current flows in the treated, roughened foil surface that bonds to the resin. John Coonrod's Rogers technical column shows that this roughness raises conductor loss and changes phase response, and that the effect depends on frequency and dielectric thickness. Record the exact foil product (standard ED, reverse-treated, VLP or HVLP) beside the laminate name. The same resin with a different foil is a different loss budget. HILPCB's high-speed PCB route specifies low-profile copper and verifies loss with VNA measurement from DC to 40 GHz.
5. Is a skewed differential pair a material problem?
It can be. Woven E-glass has a much higher Dk than the epoxy or hydrocarbon resin around it (roughly 6 against 3). A trace that runs along a glass bundle sees a higher local Dk than its partner running over a resin-rich window. As a bounding case in stripline, local Dk of 3.8 against 3.5 gives:
That is larger than the 40 ps unit interval of 25 Gb/s NRZ. Real pairs usually see a partial average, but the worst-case alignment is what closes the eye on long links.
Three countermeasures, in order of cost:
- Glass style. Open styles such as 7628, 2116 and 1080 leave large resin windows. Spread or flattened styles such as 1067, 1078 and 1086 fill the gaps more evenly. The data sheet lists available styles and resin content per style; the pressed construction must name the style used.
- Routing angle. A trace routed at angle θ to the weave moves sideways by one weave pitch p every p / tan θ of length: 8.1p at 7° and 19.1p at 3°. For a 0.5 mm pitch, that is about 4 mm and 9.5 mm. Over a long link, both traces then sample glass and resin in similar proportions. HILPCB's high-speed route uses ±7° routing or spread glass for fiber-weave skew.
- Panel rotation. Rotating the artwork on the panel gives the same averaging without changing the routing, at a cost in material use.
Part 2: Construction and lamination
6. What do resin content and resin flow tell a stackup designer?
Resin content (RC, % by weight) sets how much resin a prepreg ply carries. Resin flow (%) indicates how much of it moves under heat and pressure before gelling. During lamination that resin fills every copper-free area on the two layers it bonds. A high-RC style such as 106 or 1080 can fill dense etched signal layers. A low-RC style such as 7628 gives thickness and dimensional stability, but it can leave resin-starved voids next to heavy copper.
The data sheet gives RC and nominal pressed thickness per glass style, measured over bare cores. It cannot give the thickness over your copper pattern. That is the subject of Question 7.
7. Why doesn't "core + prepreg thickness" equal the finished board?
Resin moves into the copper-free areas. A first-order estimate for a prepreg between two copper layers is:
where R is the residual copper ratio of each facing layer. For a 100 µm prepreg:
| Facing layers | Copper fill (µm) | Estimated dielectric (µm) |
|---|---|---|
| 35 µm plane (R = 0.8) + 35 µm signal (R = 0.3) | 7.0 + 24.5 = 31.5 | 68.5 |
| 105 µm signal (R = 0.3) + 35 µm plane (R = 0.8) | 73.5 + 7.0 = 80.5 | 19.5 |
The second row is a resin-starvation warning. A 19.5 µm gap between heavy copper and a plane is too thin to hold voltage and to fill reliably. The fabricator will add plies or change to a higher-RC style. Specify the finished dielectric thickness and impedance targets. Let the fabricator choose the plies from its measured press-out data, then check the proposed stackup it returns. HILPCB's multilayer PCB route correlates field-solver models with controlled-impedance coupons, and its sequential-lamination cycles run with resin flow typically 10–20%.
8. What makes a mixed-material (hybrid) stackup different?
Hybrid boards are common in RF designs. A typical example uses an RO4000-series core for the antenna layers and FR-4 for digital control. Three properties have to agree:
- Cure cycle. Each resin system has its own lamination temperature, pressure and dwell. One press cycle has to sit inside both windows, or the bonding prepreg has to be chosen to match.
- Z-axis expansion. Different post-Tg expansion strains via barrels that cross the interface during reflow and thermal cycling.
- Hole-wall preparation. PTFE and some ceramic-filled systems need plasma or special activation before plating, while epoxy uses conventional desmear. A barrel that crosses both materials needs a preparation route that works on both.
Ask the fabricator to name the bonding layer, the press cycle and the hole-wall preparation for your exact combination, and ask what qualification evidence exists for it, such as microsection after thermal stress. HILPCB builds Rogers PCB hybrids with RF-critical layers in Rogers and the rest in FR-4.
Part 3: Thermal data: compare definitions before ranking
9. Which matters more, Tg or Td?
Neither one decides the choice alone. They measure different events:
| Property | Isola 370HR value | Method |
|---|---|---|
| Tg (glass transition) | 180 °C | DSC, IPC-TM-650 2.4.25C |
| Td (decomposition) | 340 °C | TGA, 5% mass loss, 2.4.24.6 |
| T260 / T288 | 60 min / 30 min | TMA, copper removed, 2.4.24.1 |
| Z-CTE below / above Tg | 45 / 230 ppm/°C | TMA |
| Total Z expansion, 50–260 °C | 2.8% | TMA |
Source: Isola 370HR data sheet (April 2021), p. 2, typical values.
Tg marks where the resin softens and Z-expansion jumps from 45 to 230 ppm/°C. Td marks where 5% of the mass has decomposed. Lead-free reflow peaks around 245–260 °C, far above Tg for most FR-4 grades, so the board spends each reflow in the high-expansion region. That makes Z-CTE and T288 at least as important as the Tg value. Tg can also be measured by DSC, TMA or DMA, and the methods give different numbers for the same resin. Compare Tg only between entries measured the same way.
10. Can two Td values be compared directly?
Only when the mass-loss criterion matches. The AGC NF-30 technical data sheet (2024-08, p. 4) lists Td 515 °C at 2% loss and 530 °C at 5% loss for the same material. A 2%-loss value from one vendor ranked against a 5%-loss value from another is not a valid comparison.
11. What do T260 and T288 add?
They are the time a copper-free specimen at 260 °C or 288 °C survives in TMA before it delaminates. They describe resistance to extended exposure at those temperatures. They are useful for comparing constructions headed for several lead-free reflows or rework. They are not a cycle-life rating for a plated board. Via reliability is better shown by IST or thermal-cycling microsections on coupons built with the real stackup. HILPCB's multilayer route reports IST results in the 200–500 cycle range.
12. How should Z-axis CTE be read?
Check which axis, which temperature interval, and whether it is a coefficient (ppm/°C) or a total expansion (%). Isola gives 45/230 ppm/°C split at Tg plus 2.8% total over 50–260 °C. NF-30 gives 30 ppm/°C over 50–150 °C only. The two cannot be ranked from these rows.
The total figure matters most for thick boards. On a 1.6 mm board, 2.8% is 44.8 µm of Z growth from 50 to 260 °C. Over the same 210 °C, a copper barrel (about 17 ppm/°C) grows only about 5.7 µm. The plating has to absorb the difference, and it concentrates at the barrel knee and inner-layer connections. Thicker boards and higher aspect ratios push the strain up. Low-Z-CTE materials matter most for thick boards and for areas under large BGAs.
Part 4: Reliability and process compatibility
13. What is CAF, and what does an "anti-CAF" entry mean?
Conductive anodic filament (CAF) growth is copper migrating along a glass-fiber/resin interface between two conductors at different potentials, driven by moisture and voltage. It is a field failure that appears after months or years. The usual sign is a resistance drop between adjacent vias or a via and a plane, and a microsection shows a filament following the glass.
An anti-CAF claim means something only together with its test conditions: temperature, humidity, bias voltage, hole-wall spacing and duration (for example to IPC-TM-650 2.6.25). A pass at a 0.5 mm wall-to-wall spacing does not cover a 0.25 mm design. The board process matters as much as the resin. Drilling damage, wicking along fibers and desmear quality open the path that CAF follows. For dense via fields under BGAs, check that the test spacing in the material data is at or below your minimum wall-to-wall spacing, and ask the fabricator how it limits wicking. HILPCB's multilayer route lists CAF-resistant materials and processes for this case.
14. How should moisture absorption and baking be used?
Absorbed water turns to steam during reflow. In thick, high-layer-count boards it can cause blistering or delamination. The data-sheet absorption value (% weight gain under a defined immersion or humidity condition) lets you compare resins. It does not give a bake schedule. Bake time and temperature for finished boards depend on thickness, surface finish (some finishes degrade with long bakes) and storage history. Take them from the fabricator's and assembler's procedure, and record vacuum-sealed packaging and storage time with the lot.
15. Can laser-drill compatibility be inferred from "high-speed material"?
No. CO₂ lasers ablate resin well but glass poorly. Heavy glass in the build-up dielectric leaves protruding fibers and irregular microvia walls. Some low-loss resin systems also absorb CO₂ wavelengths less well, which pushes the process toward UV lasers or different parameters. Check whether the data sheet names laser-drillable prepreg styles. Then confirm that the fabricator has a qualified laser window for that exact prepreg and thickness. HILPCB's HDI PCB route drills laser microvias from 0.05 mm with UV and CO₂ systems.
Part 5: Application requirements beyond one number
16. Do CTI and dielectric strength set the insulation spacing?
They feed into it but do not set it. CTI (comparative tracking index, IEC 60112) ranks resistance to surface tracking under contamination. It places the material in a group used by safety standards: Group I at CTI ≥ 600, II at 400–600, IIIa at 175–400, IIIb at 100–175. The required creepage then depends on working voltage, pollution degree and the product standard (for example IEC 62368-1 or IEC 60664-1). Dielectric strength (kV/mm) describes through-thickness breakdown of a thin specimen under a defined test. Wide spacings break down at lower average fields than thin specimens, so this value does not scale linearly to them. Record both properties with their methods and let the product safety requirement set the spacing.
17. Which flex data matters for dynamic bending?
For a hinge or a cable that keeps moving:
- Copper type. Rolled-annealed (RA) copper has a grain structure elongated along the foil and survives far more bend cycles than electrodeposited (ED) copper, which has a columnar grain. Route the bend region so the RA grain direction runs along the trace.
- Construction. Adhesiveless polyimide removes the acrylic or epoxy adhesive layer. That makes the stack thinner and keeps the copper closer to the neutral axis.
- Stack symmetry. A single copper layer placed at the neutral axis, with cover film balanced on both sides, gives the lowest copper strain.
Peel strength shows adhesion, and flex endurance (MIT fold or IPC-TM-650 2.4.3) shows cycle behavior under one test geometry. Neither replaces a cycle test at your bend radius. HILPCB's flex PCB route reviews these choices with the stackup.
18. Is a higher MCPCB thermal conductivity always better?
The insulating dielectric between the copper circuit and the aluminum base is usually the bottleneck. Its thermal resistance per area is R = t / (k · A). For 1 cm²:
| Dielectric | Thickness | k (W/m·K) | R (K/W per cm²) |
|---|---|---|---|
| A | 100 µm | 2.0 | 0.50 |
| B | 75 µm | 3.0 | 0.25 |
Halving R means halving the LED-to-base temperature rise across the dielectric. Check whether the quoted k is for the dielectric alone or for the whole board. Prefer a thermal-impedance value (K·cm²/W) measured to a stated method. A thinner dielectric also reduces breakdown margin, so trade it against the isolation test voltage. HILPCB's metal-core PCB route covers these dielectric options.
19. How should compliance declarations enter the review?
Ask for declarations that cover the finished board, not only the base laminate. EU RoHS restricts 10 substances (lead, mercury, cadmium, hexavalent chromium, PBB, PBDE and four phthalates). "Halogen-free" for laminates usually refers to IEC 61249-2-21: bromine ≤ 900 ppm, chlorine ≤ 900 ppm, total ≤ 1500 ppm. REACH SVHC declarations refer to the ECHA candidate list as of a date, so record that date. Solder mask, legend ink and surface finish need their own declarations. HILPCB offers a halogen-free PCB route.
20. How can two supplier stackup proposals be compared fairly?
Line them up by construction, not by the trade name in the title row:
| Field | Proposal A | Proposal B | Comparable? |
|---|---|---|---|
| Laminate and prepreg family, glass style | Named | "FR-4 equivalent" | No, until B names the product |
| Foil type and thickness | HVLP, 18 µm | Not stated | Loss cannot be compared |
| Finished dielectric per layer | Listed with tolerance | Total thickness only | Impedance cannot be checked |
| Dk input and its source | Design Dk, named method | Single-point 1 GHz | Different bases |
| Impedance verification | TDR coupon, ±5% | ±10%, method unstated | Different acceptance |
| Thermal data | Tg method and Td criterion stated | Tg only | Incomplete |
If a substitute is proposed, ask for the same table for the substitute and approve it in writing before the order. A cheaper quote built on an unnamed construction is cheaper for an unspecified product.
What to send with a stackup or material RFQ
- Target finished dielectric thickness per layer, impedance targets with tolerance, and the reference layers for each line.
- The exact laminate and prepreg product names you designed with, the foil profile, and the Dk/Df rows you used, including method and frequency (see the model-input record).
- Glass-style or routing-angle requirements for skew-sensitive pairs.
- Thermal and reliability requirements stated as tests: number of reflows, IST or thermal-cycling coupons, CAF spacing.
- Whether substitutes are allowed, and who approves them.
- Required reports: stackup confirmation, TDR coupon report, microsection, VNA data.
Use stackup documentation to connect the accepted proposal to the fabrication drawing.
HILPCB builds 4–64 layer multilayer PCBs, high-speed PCBs in Megtron, Tachyon and other low-loss families, and Rogers PCBs including Rogers + FR-4 hybrids. Coupon TDR verifies impedance to ±5% when specified (±10% standard). Sample VNA testing runs to 40 GHz, and IST and microsection reports are available on request. Send your target stackup and material list when you request a quote for an engineering stackup review.
Frequently Asked Questions
My TDR reads low impedance. Does that mean the real Dk is higher than the data sheet?
Not on its own. In the 50 Ω microstrip example above, a pressed dielectric only 25 µm thinner than modeled drops the line to 46 Ω with Dk unchanged. Measure the coupon cross-section first, re-run the solver with the actual height and trace width, and only then attribute the remaining difference to Dk.
Can an impedance coupon verify Df?
No. A TDR impedance value depends almost entirely on Dk and geometry and is nearly insensitive to Df. Loss needs a separate measurement, such as VNA insertion loss on lines of two different lengths, with conductor roughness modeled separately so its loss is not counted as dielectric loss.
Why might a fabricator decline to use the exact prepreg styles on my drawing?
The required resin fill depends on your copper pattern, which the data sheet cannot know. A prepreg that works over a plane can starve next to 105 µm signal copper (19.5 µm estimated in Question 7). Specify finished dielectric thickness and impedance, and review the plies the fabricator proposes from its press-out data.
Is a halogen-free laminate automatically better for high-reliability boards?
No. Halogen-free describes bromine and chlorine content to IEC 61249-2-21. Many halogen-free resins use different fillers, which change drilling behavior, Z-expansion and moisture absorption. Qualify a halogen-free construction on its own thermal, CAF and drilling data instead of assuming parity with the brominated grade it replaces.